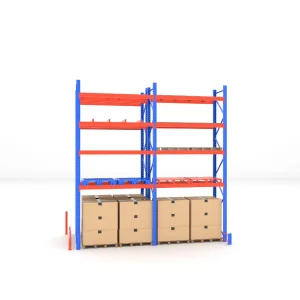
Engineered for maximum weight capacity, structural safety compliance, and optimized space efficiency.
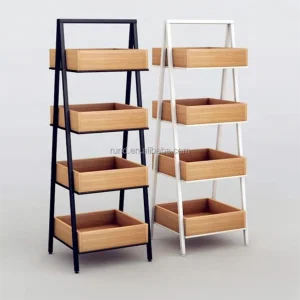
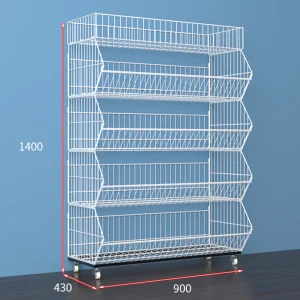
Established in 2014, Nanjing Dulis Warehouse Equipment Co., Ltd. (operating globally under the brand DuraRacks) is a premier industrial rack manufacturer headquartered in Nanjing, China. Boasting over 12 years of industry experience and 9 years of direct export experience, our facility spans a modern industrial building area of 38,000 square meters. We specialize in high-capacity pallet racking, drive-in systems, and automated storage solutions, generating an annual export revenue of $32 million USD.
As pioneers of high-density heavy storage technology in East China, we utilize superior cold-rolled structural steel to manufacture industrial storage racks engineered for structural integrity, durability, and seismic resilience. From static warehouse racks to dynamic automated storage systems, our structural steel racks are built to exceed performance metrics under heavy loads, ensuring safe operation within high-density facilities, logistics hubs, and global industrial applications.
A look into our state-of-the-art facility processes, ensuring top-tier reliability for global supply chains.
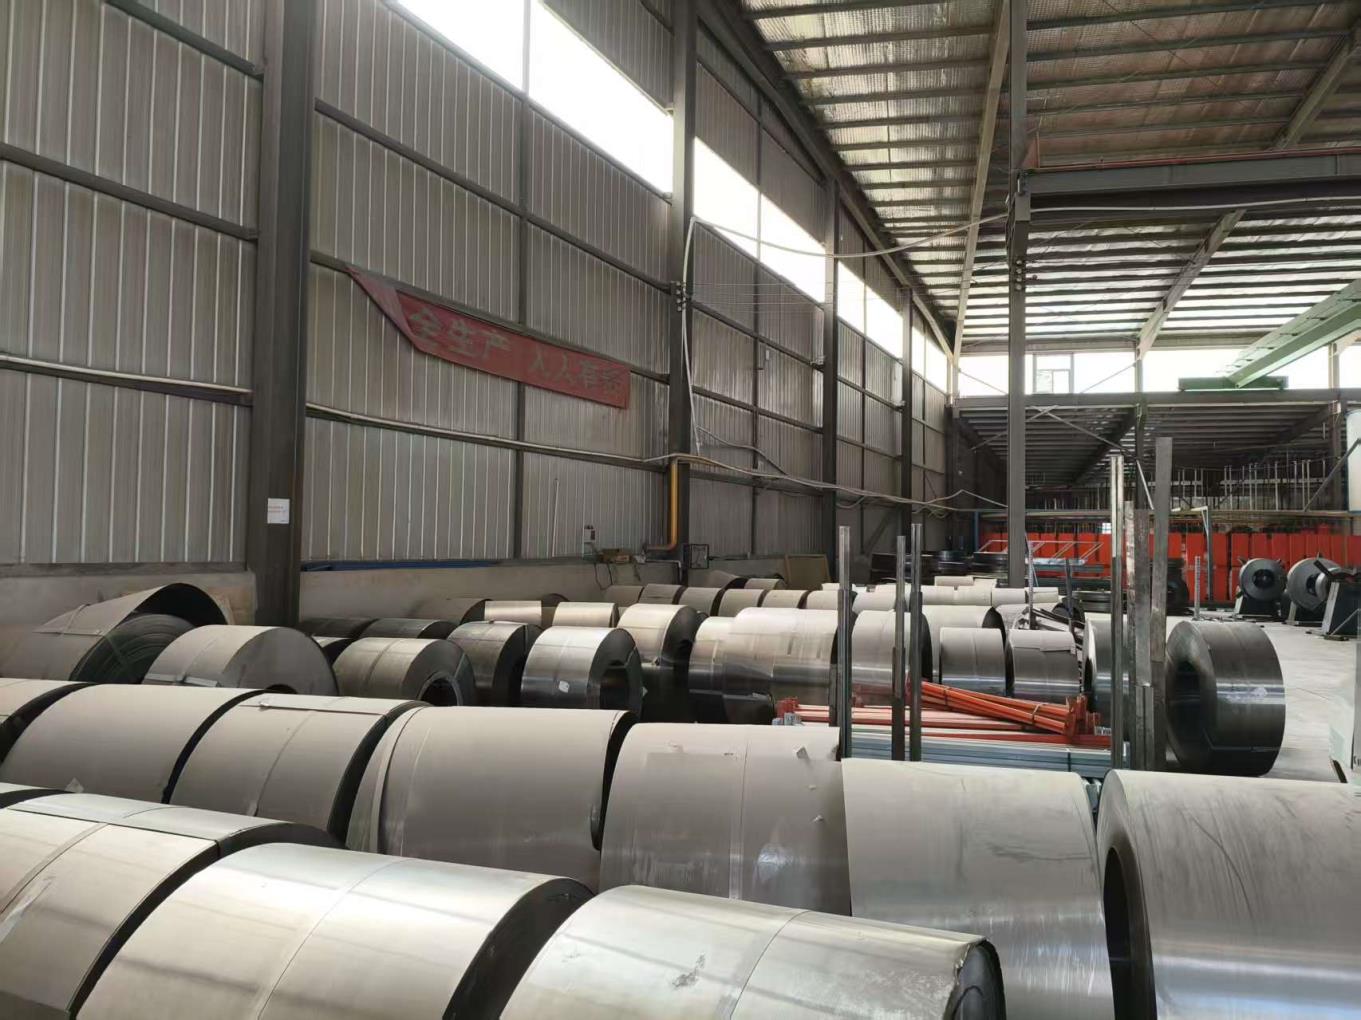
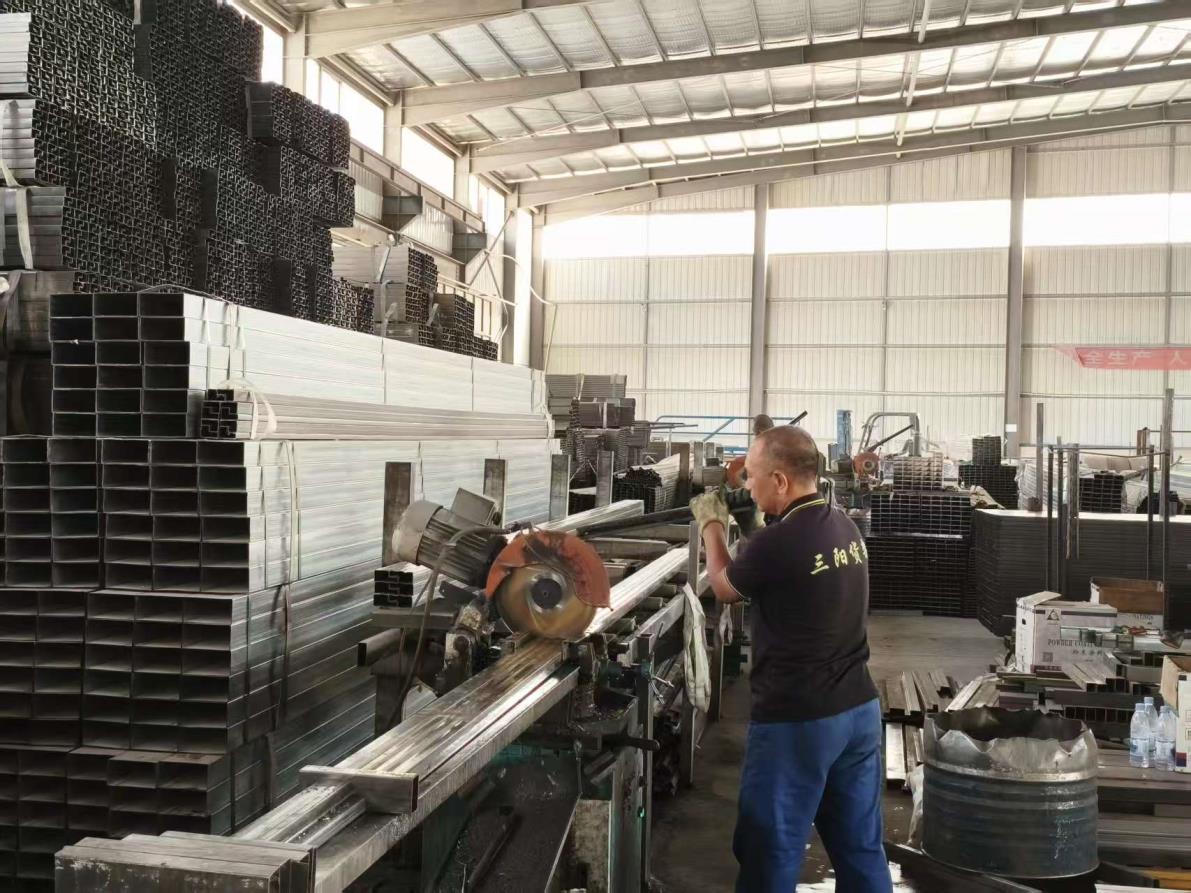
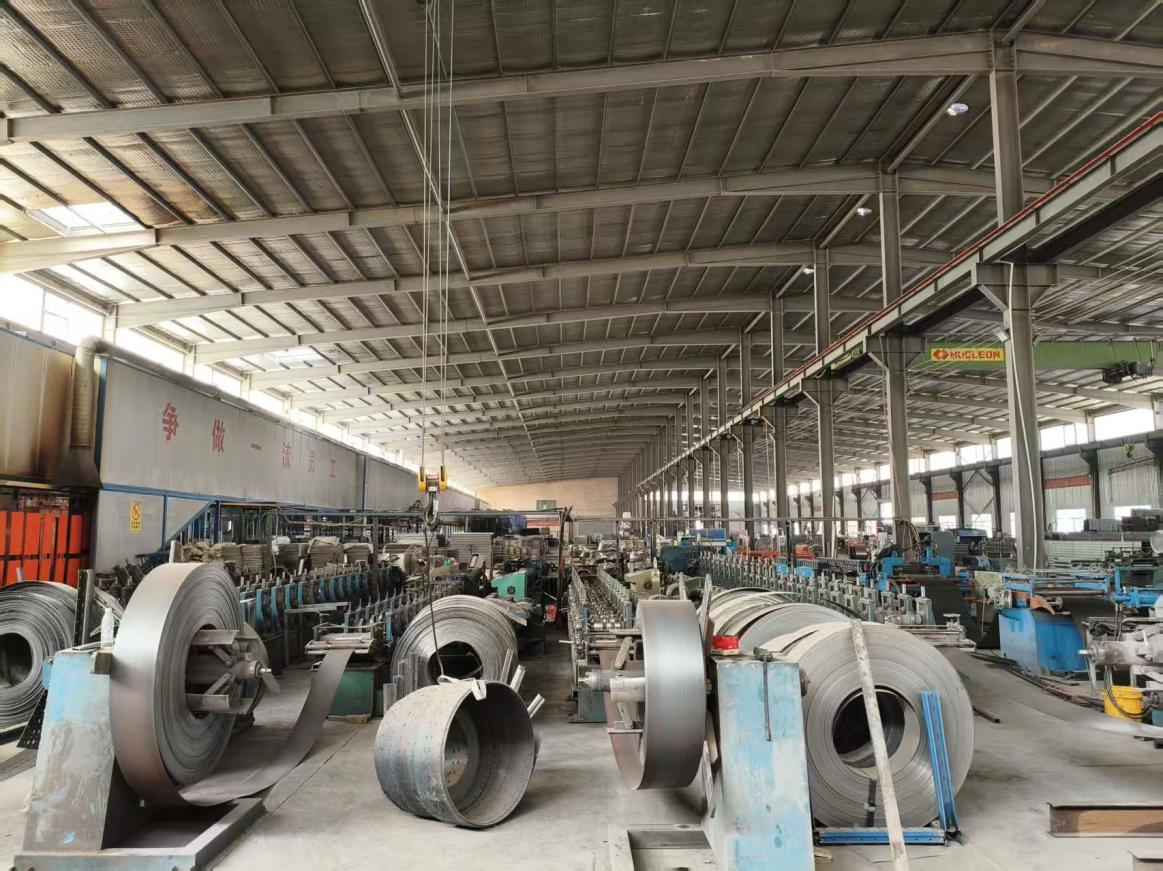
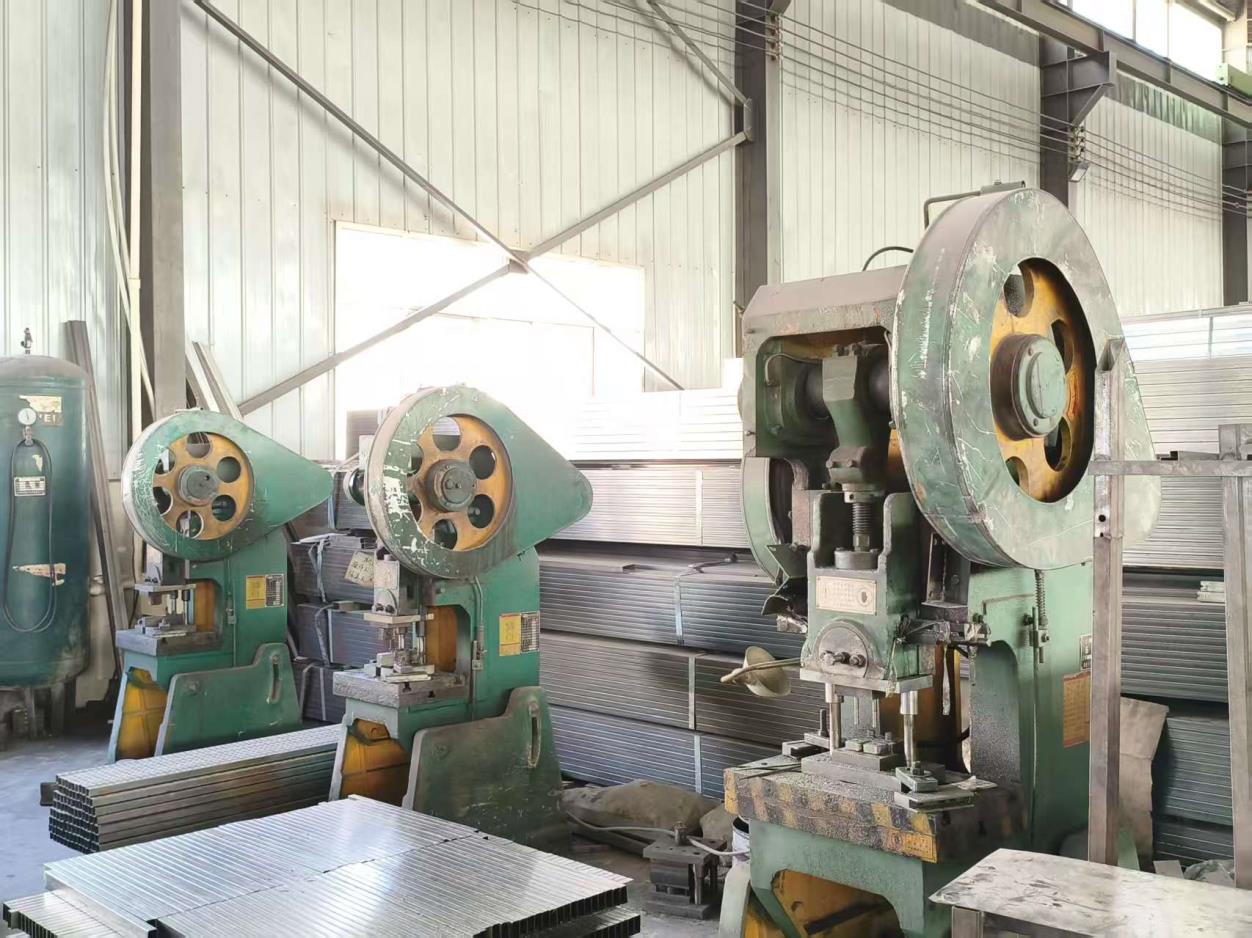
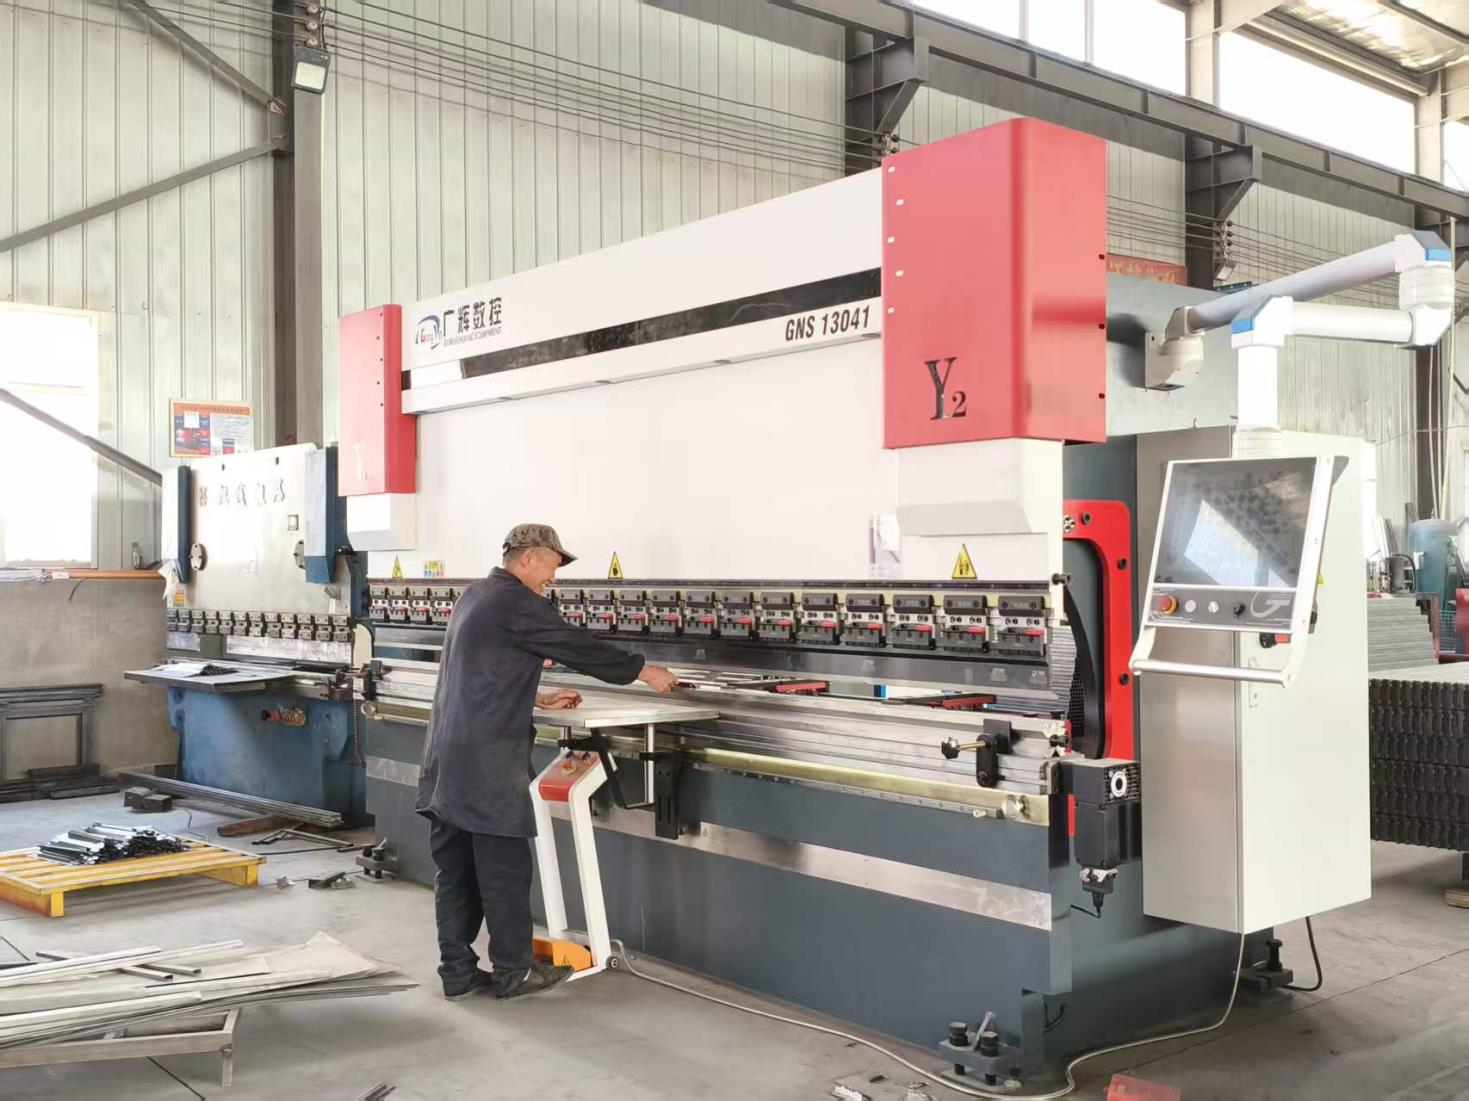
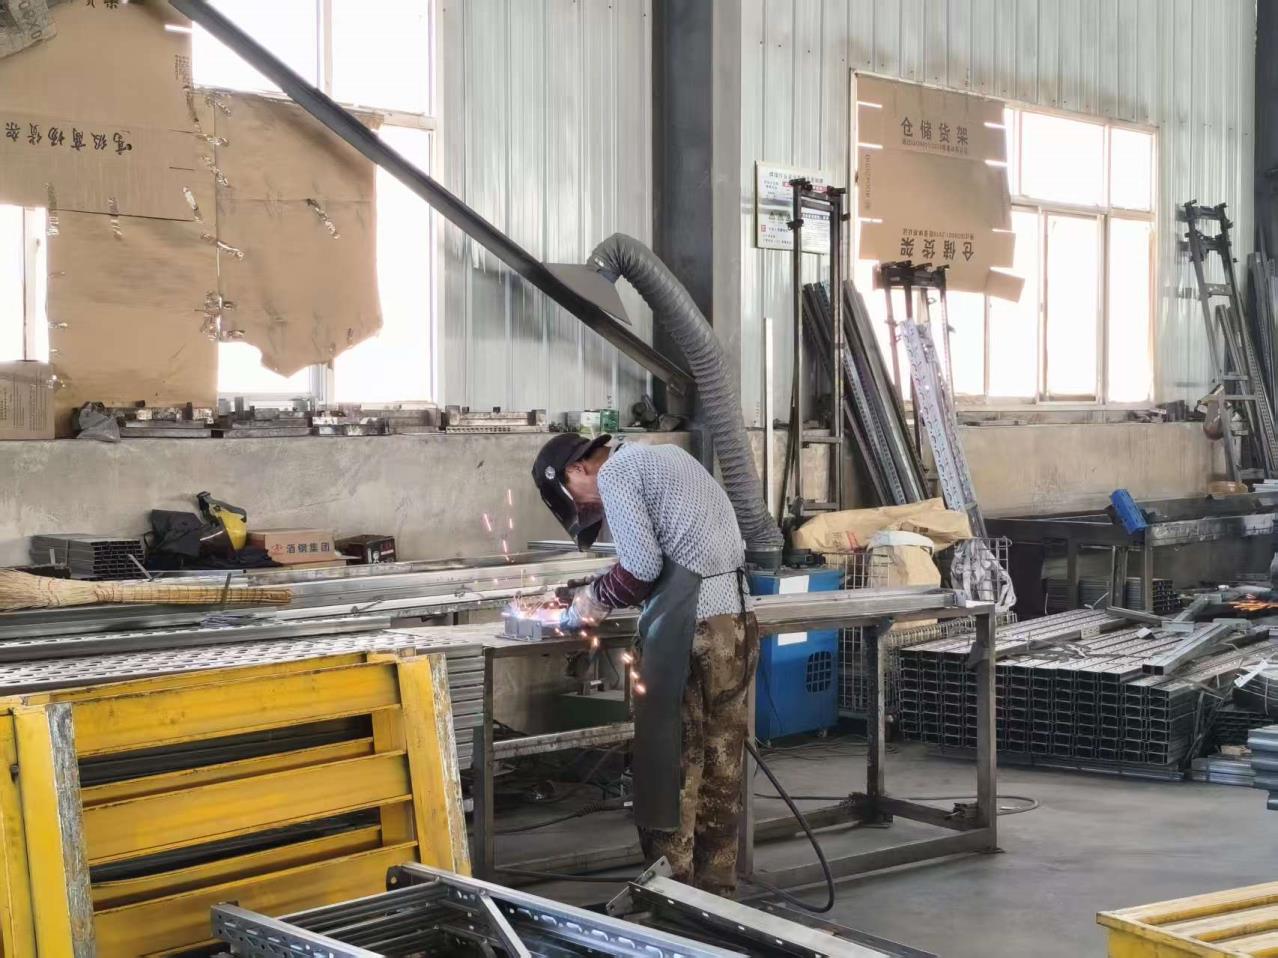
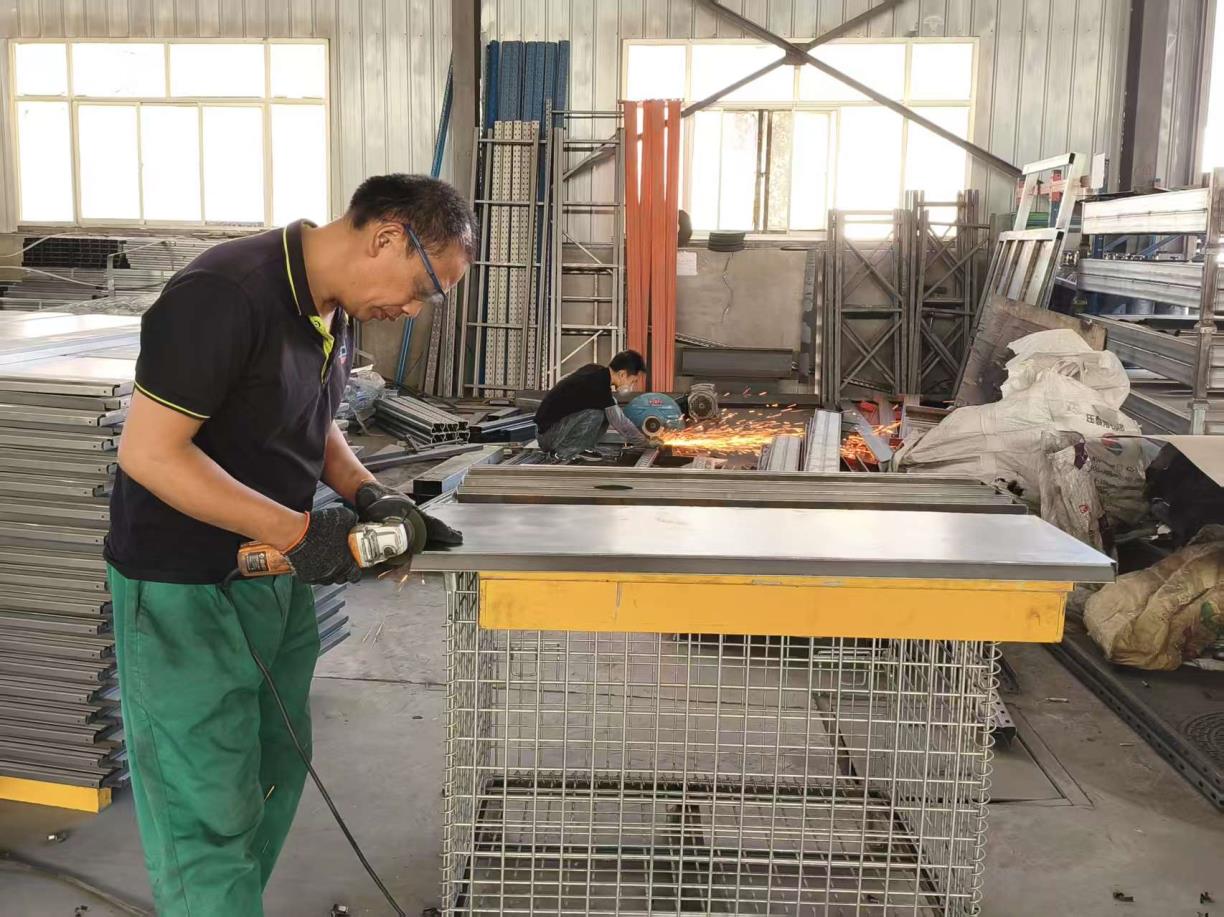
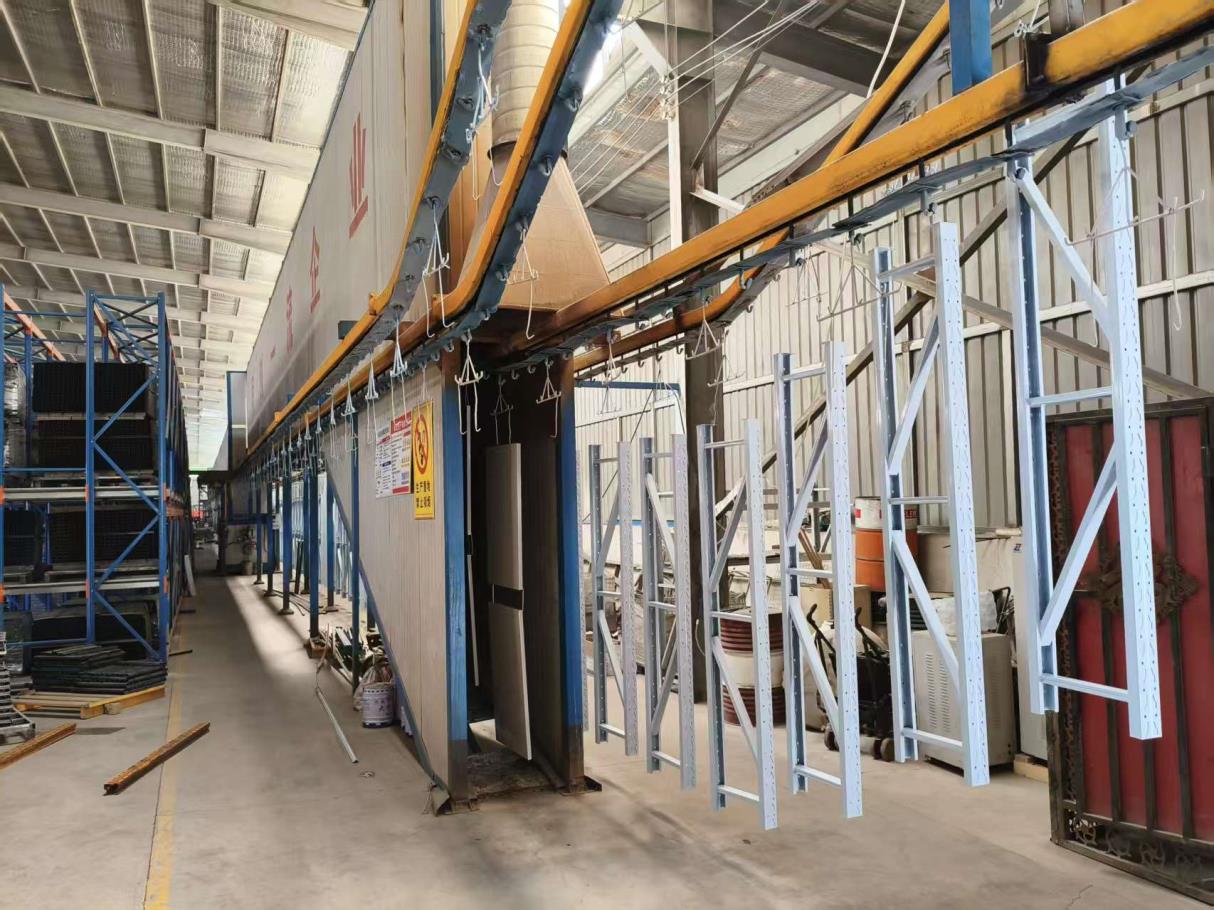
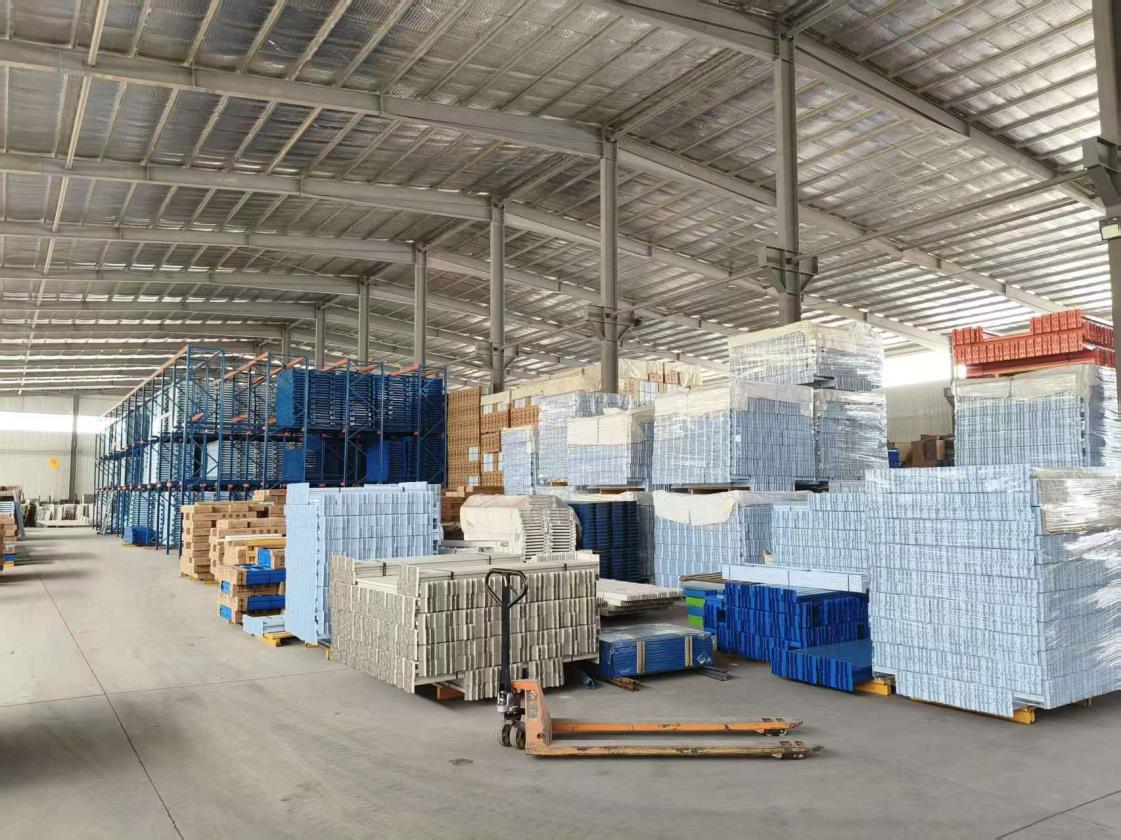
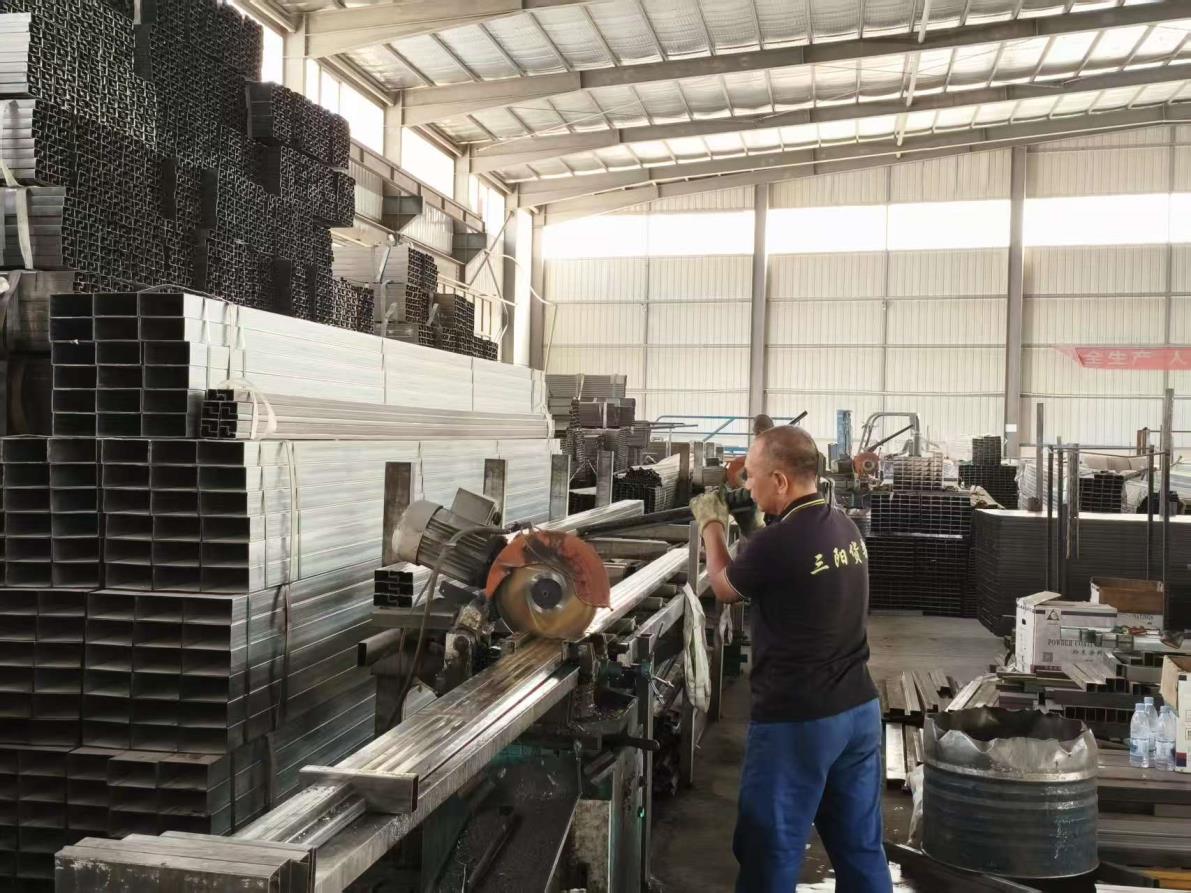
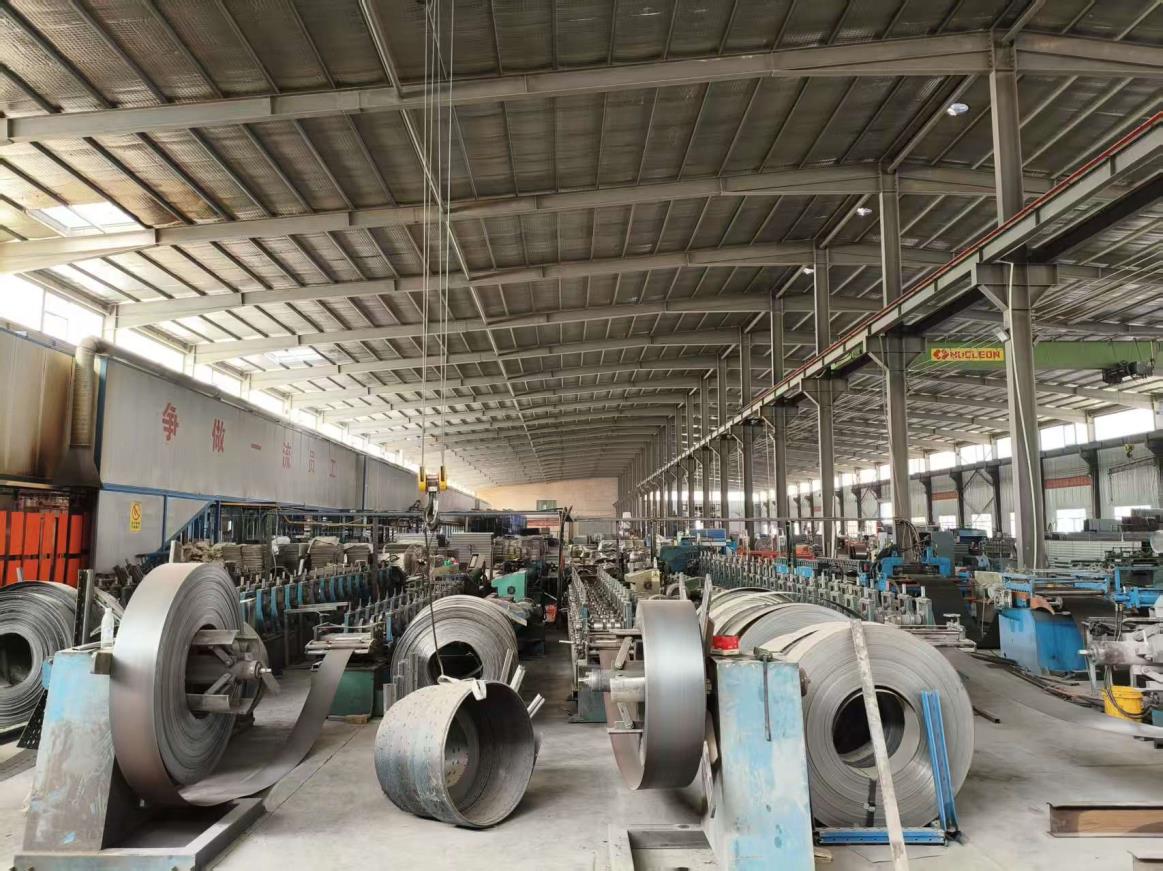
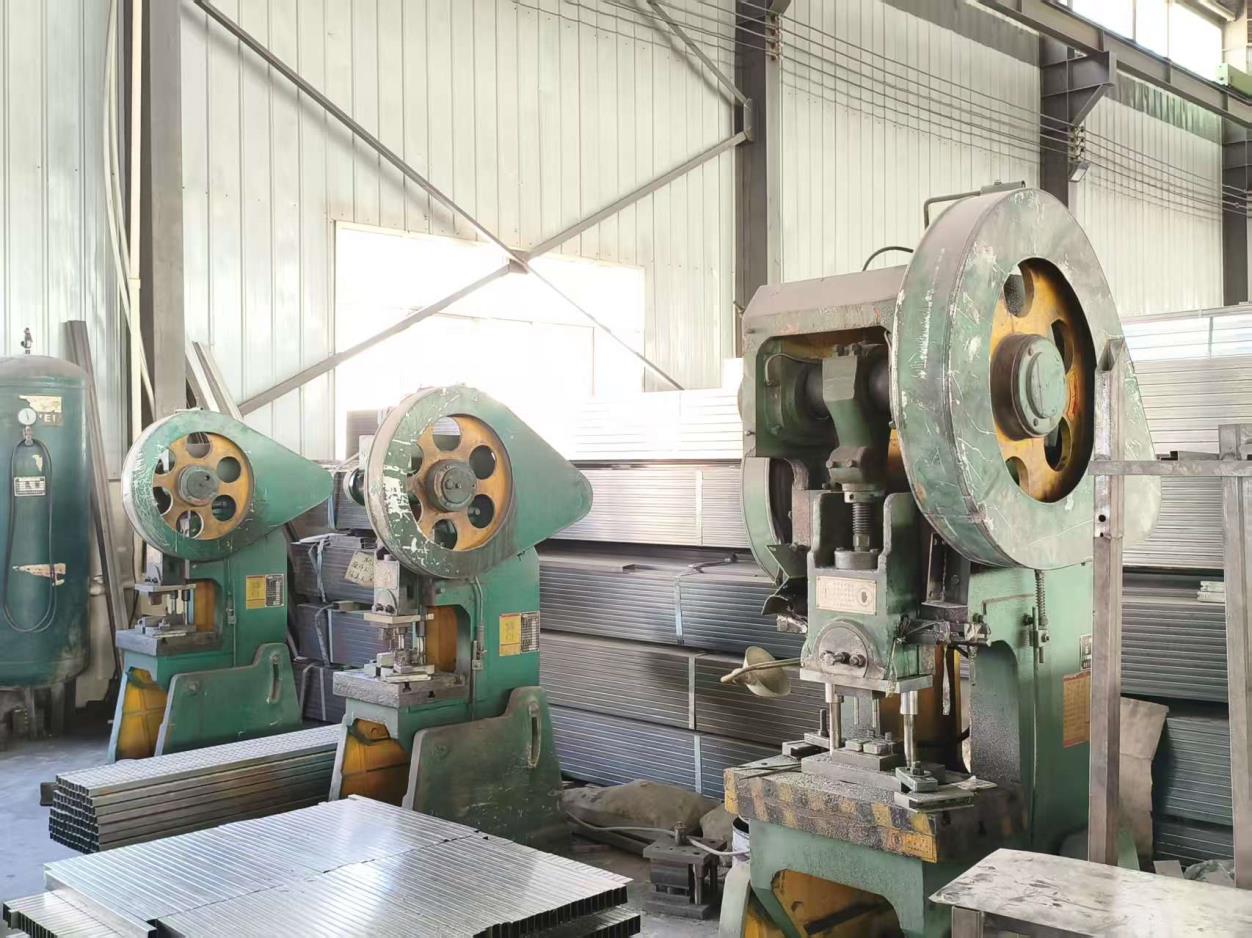
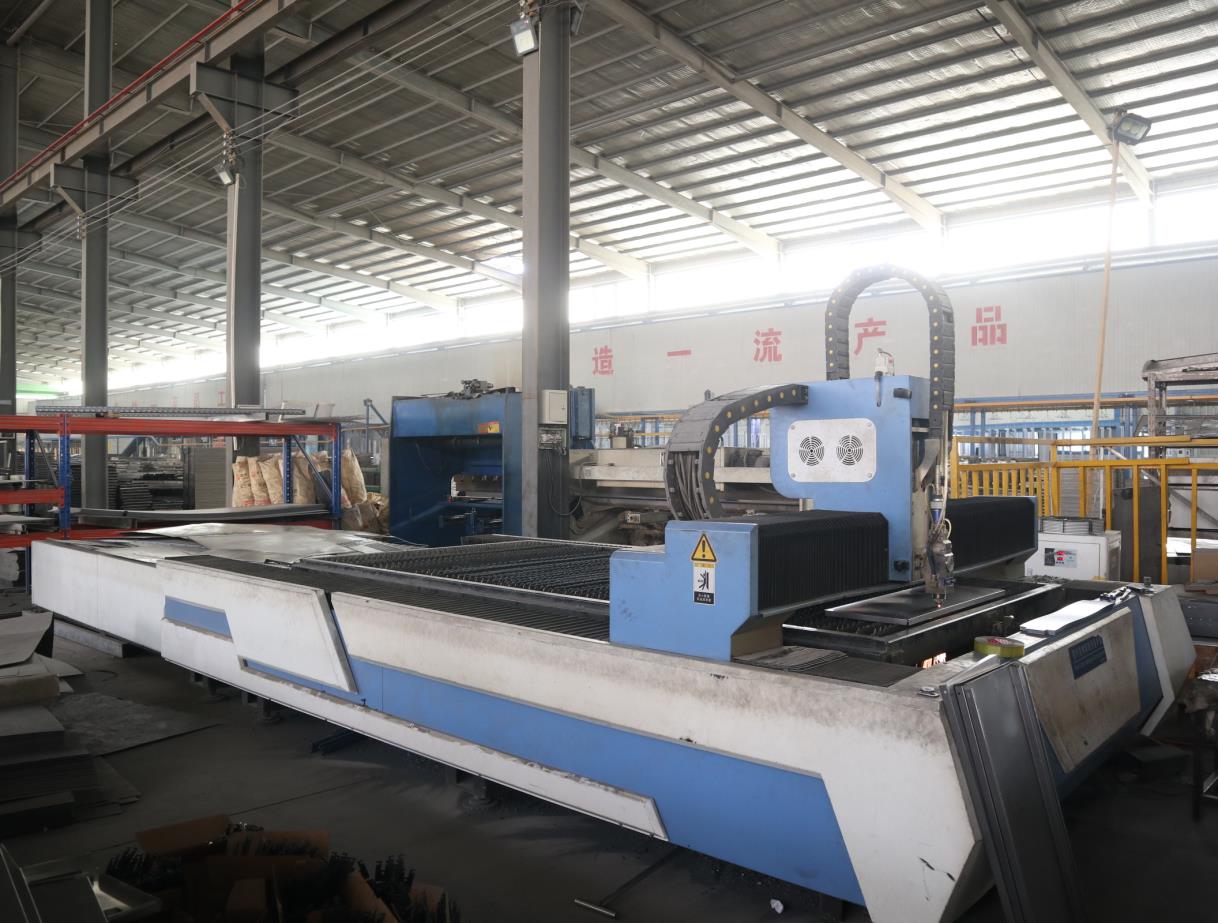
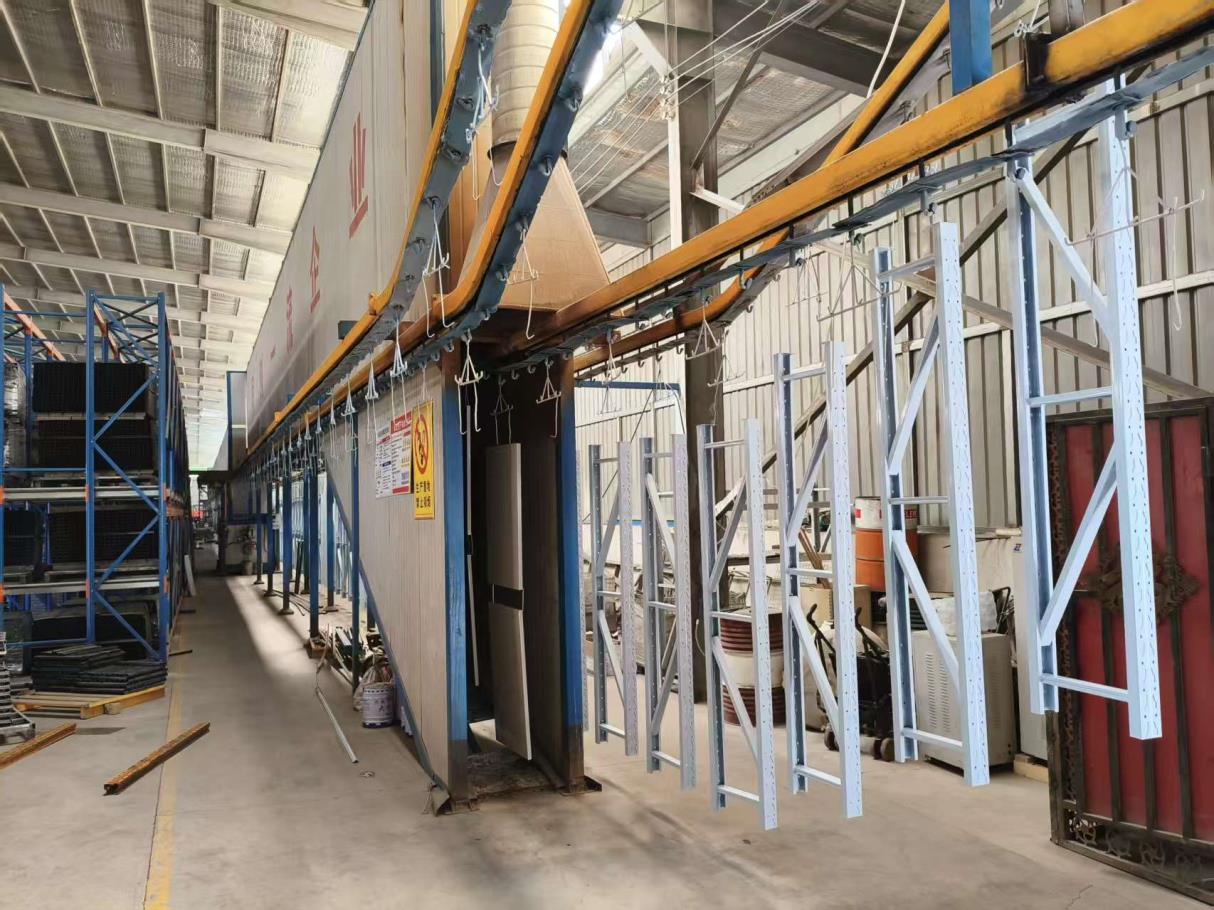
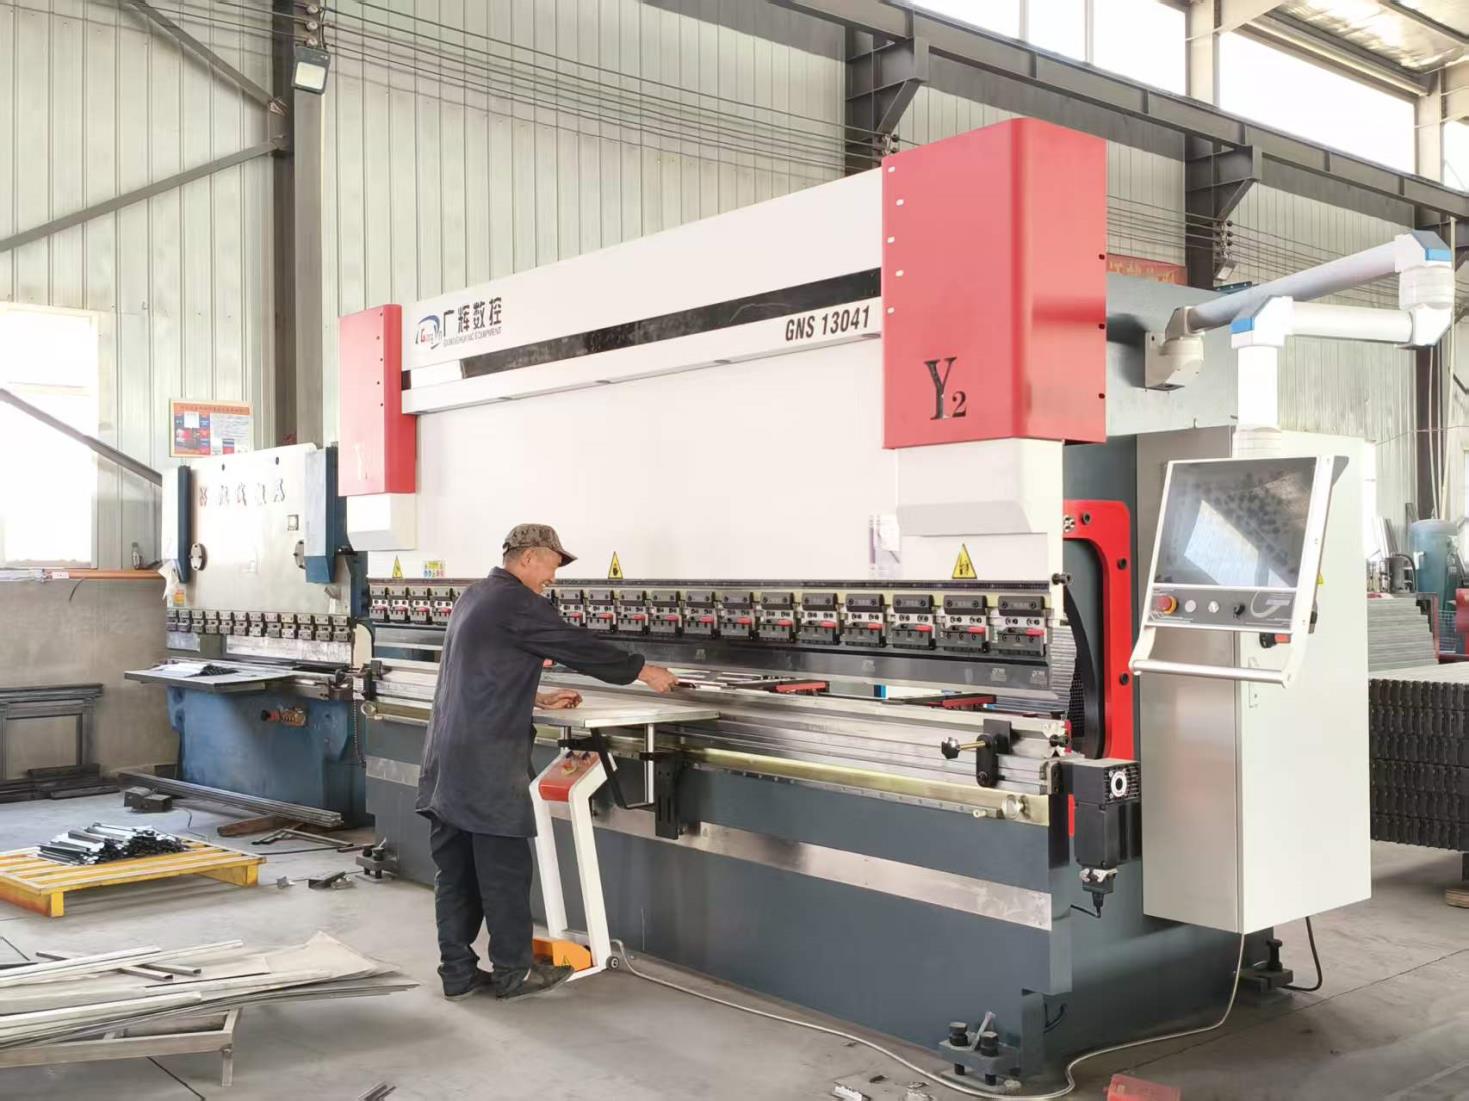
Quality and structural integrity form the bedrock of our manufacturing philosophy. Our dedicated team of 45 certified QA personnel implements rigorous quality control processes aligned with ISO9001, CE, and FEM standards. Every batch undergoes comprehensive product inspection methods, including ultrasonic weld flaw detection, mechanical tensile testing, static and dynamic load capacity testing, and salt spray corrosion resistance evaluation. This guarantees that every warehouse racking profile and beam shipped to our clients can safely support its intended load capacity under real-world operating conditions.
Understanding the unique structural and supply chain advantages that position China as a global leader.
We source structural steel (primarily Q235B and Q355B grades) from China's top state-owned steel mills. This ensures consistent mechanical properties, high yield strengths, and excellent weldability. This material quality is critical for components that support thousands of kilograms per pallet.
Equipped with a team of 68 expert engineers, DuraRacks performs rigorous Finite Element Analysis (FEA) to simulate load distributions, seismic forces, and wind pressures (for rack-clad structures). We provide custom CAD layouts and BIM modeling before production to optimize spatial efficiency.
Our 38,000㎡ manufacturing facility utilizes state-of-the-art automated cold rolling lines, continuous punching machinery, laser-cutting technology, and eco-friendly electrostatic powder-coating lines to produce massive quantities of racking structural profiles without sacrificing precision.
Located near East China's logistics corridors, DuraRacks coordinates with over 1,200 qualified supply chain partners. We streamline export documentation, custom-clearance procedures, container loading, and ocean freight logistics to ensure cargo arrives safely in North America, Western Europe, and Australia.
Our heavy storage shelves are built to comply with major international specifications, including the Rack Manufacturers Institute (RMI) standards in the US, European FEM 10.2.02 regulations, and Australian standard AS4084-2012, guaranteeing safe warehouse operations.
By optimizing design efficiency and leveraging China's dense industrial manufacturing ecosystem, we offer high-grade, durable racking systems that minimize capital expenditure per pallet position, yielding high ROI for logistics operators and warehouse investors.
Providing specialized warehouse layouts and heavy storage infrastructure across various commercial sectors.
High-density selective pallet racking and drive-in racking systems optimize vertical space, allowing Third-Party Logistics (3PL) providers to maximize storage capacity while maintaining rapid, individual access to SKU inventories. Custom upright dimensions and load-capacity calculations prevent structure deflection under continuous warehouse forklift traffic.
Cold storage is highly expensive to build and operate. Our high-density dynamic storage racking systems, including Drive-In, Push-Back, and Radio Shuttle systems, drastically decrease cooling space requirements. Every structural component uses low-temperature resilient steel finishes to prevent brittle fracturing at sub-zero temperatures.
Engineered for storing massive dies, raw metal coils, sheet metal, and finished automotive assemblies. Cantilever racking and high-capacity mold racking allow overhead cranes and specialized forklifts to load and retrieve heavy materials safely, featuring integrated deflection alarms and heavy duty impact protection barriers.
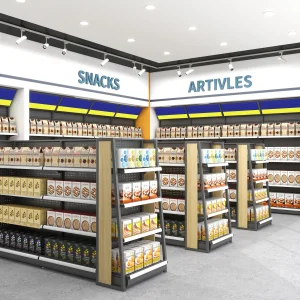
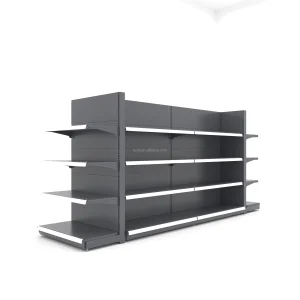
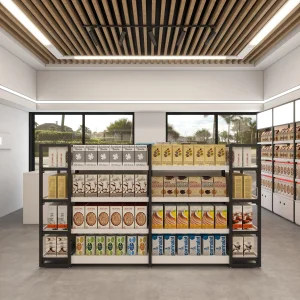
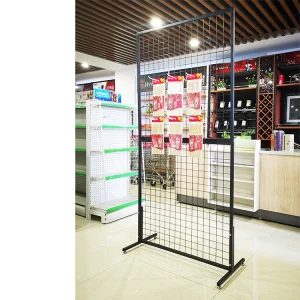
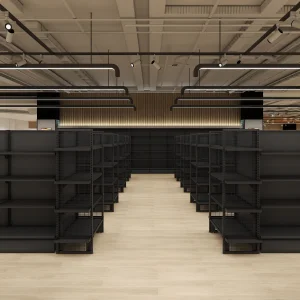
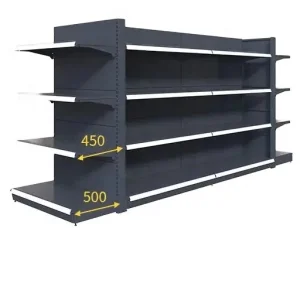
Integrating heavy-duty back-room warehouse storage with retail-ready store displays. Our customizable gondola systems and hybrid rack-display units support heavy loads (e.g., grain, oils, beverages) directly on the retail floor, ensuring visual appeal, customer safety, and robust load capacity.
How automation, green manufacturing, and smart warehouse technology are reshaping heavy-duty storage shelves.
The rapid rise of global e-commerce and immediate order-fulfillment cycles has forced businesses to transition from conventional static warehouses to highly automated logistics operations. Standard structural racks are evolving to accommodate advanced robotic machinery. Automated Storage and Retrieval Systems (AS/RS) require extreme precision in vertical column tolerance and rail alignment. Even small structural shifts or sagging beams can cause automated cranes or shuttle cars to fault, bringing fulfillment lines to a halt. At DuraRacks, our engineering teams perform Finite Element Analysis (FEA) to verify that structural frame profiles remain perfectly stable, supporting dynamic robot-assisted warehousing under heavy workloads.
Concurrently, green manufacturing practices and corporate ESG responsibilities are influencing material specifications. Global procurement departments now demand low-emission manufacturing and toxic-free finishes. In response, our facility has modernized its coating processes to utilize solvent-free electrostatic powder coating, eliminating Volatile Organic Compounds (VOCs) and hazardous waste runoff. This eco-friendly surface treatment is highly resistant to impact, UV exposure, and moisture, extending the lifespan of our heavy storage shelves in humid industrial plants and high-condensation cold chain environments.
Additionally, modular design is crucial for modern facilities. Warehouses must adapt to changing product dimensions, shifting seasonal inventory levels, and varying storage priorities. Modular, adjustable steel storage shelves allow operators to quickly modify beam heights, extend rack runs, or convert selective pallet systems into drive-in setups. This flexibility extends the usable lifetime of the racking infrastructure, reducing future capital expenditure and supporting long-term operational resilience.
Expert insights on product specifications, load limits, layout customization, and global shipping logistics.
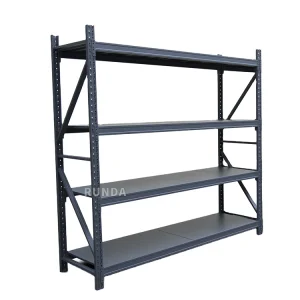
Explore our secondary line of heavy display racks, structural supports, and functional store equipment.
 DuraRacks