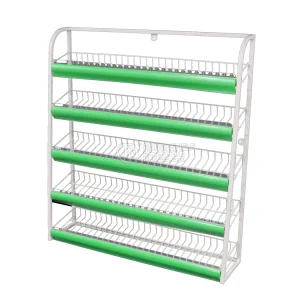
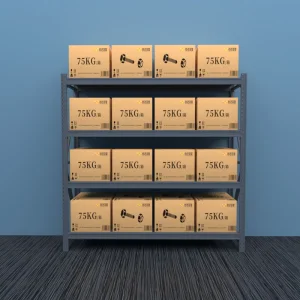
Engineered high-performance retail solutions, storage configurations, and logistics trolleys designed to optimize consumer pathways and high-density inventory storage.
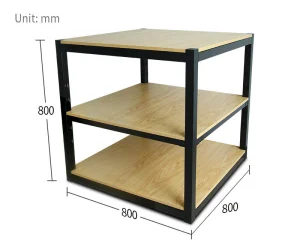
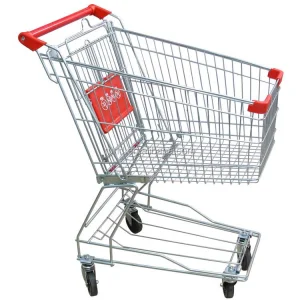
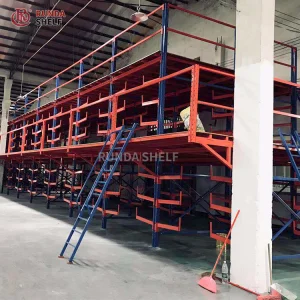
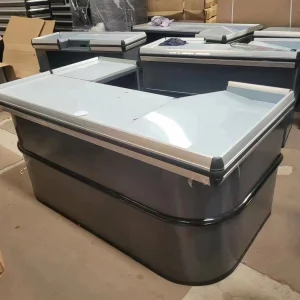
In the highly competitive arena of modern brick-and-mortar retail, structural layout planning, space utilization efficiency, and user navigation are not simply aesthetic variables—they are key drivers of commercial conversion. Supermarket shelving, gondola display racks, and specialized warehouse systems represent the core infrastructure supporting the global retail supply chain. Today's commercial shelves must withstand heavy structural loading, minimize dynamic floor footprints, maintain anti-corrosive properties, and facilitate rapid inventory management through modular design.
"For modern hypermarkets and high-volume grocery hubs, an optimized shelving ecosystem improves stock visibility by up to 35% and drastically reduces replenishment times. By focusing on engineering integrity, modern supermarket shelves serve as the physical interface between structural supply chain stability and localized consumer demand."
According to current global retail industry intelligence, the supermarket shelving sector has expanded from simple structural assembly racks into integrated retail ecosystems. Advanced manufacturers are incorporating multi-material compositions, low-energy LED illumination, sensor-driven retail elements, and integrated warehouse-to-store material handling capabilities. In the sections below, we provide a complete whitepaper-level analysis of supermarket shelves manufacturing, materials science, design methodologies, and supply-chain logistics.
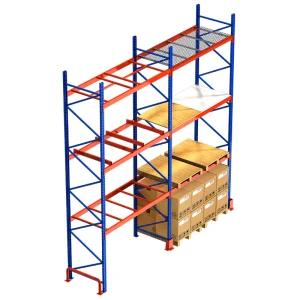
High-precision warehouse and store display racking, engineered by Nanjing Dulis Warehouse Equipment Co., Ltd. for optimal structural performance.
Purchasing agents and retail procurement managers globally recognize that sourcing commercial display structures from leading Chinese factories provides distinct efficiency advantages. These benefits extend beyond simple unit-cost reductions to encompass comprehensive vertical integration, advanced raw-material processing, and deep technological capacity.
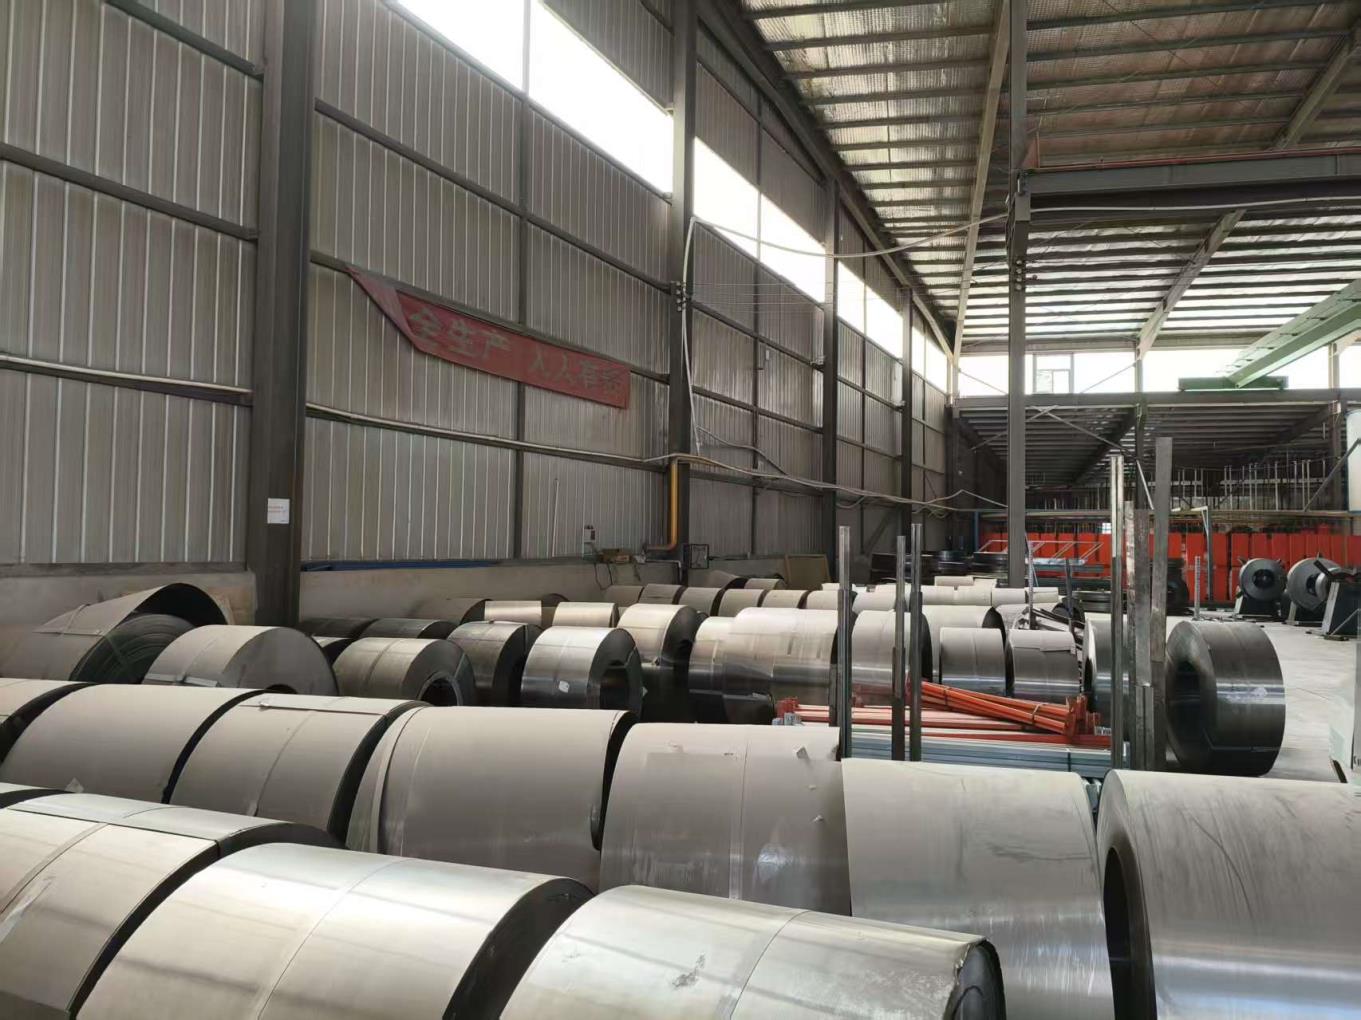
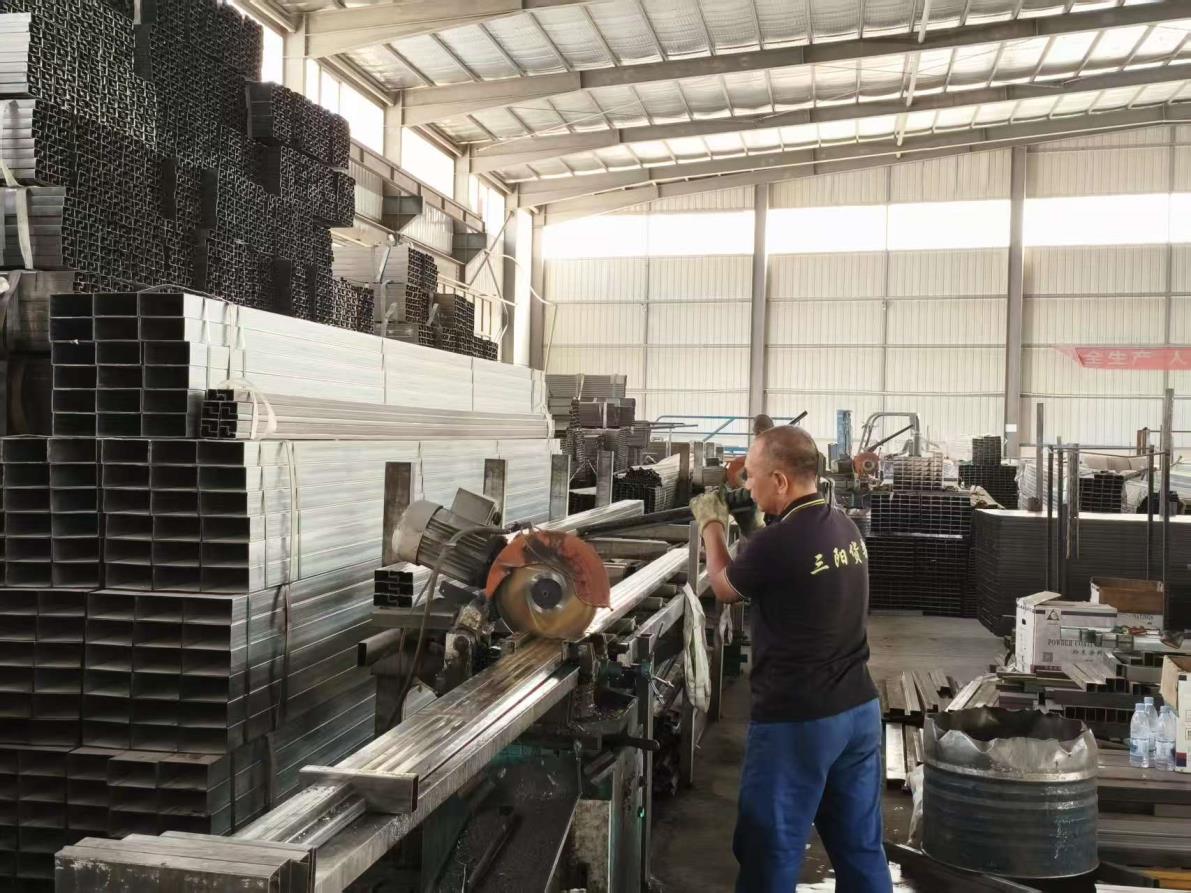
Leading companies like Nanjing Dulis (operating globally as DuraRacks) leverage direct relationships with tier-one domestic steel mills. By utilizing certified high-grade Q235B steel coils, the factory maintains constant material performance metrics. This raw material consistency prevents structural warping, supports accurate loading capacity ratings, and ensures compliance with FEM, ISO, and CE international standards.
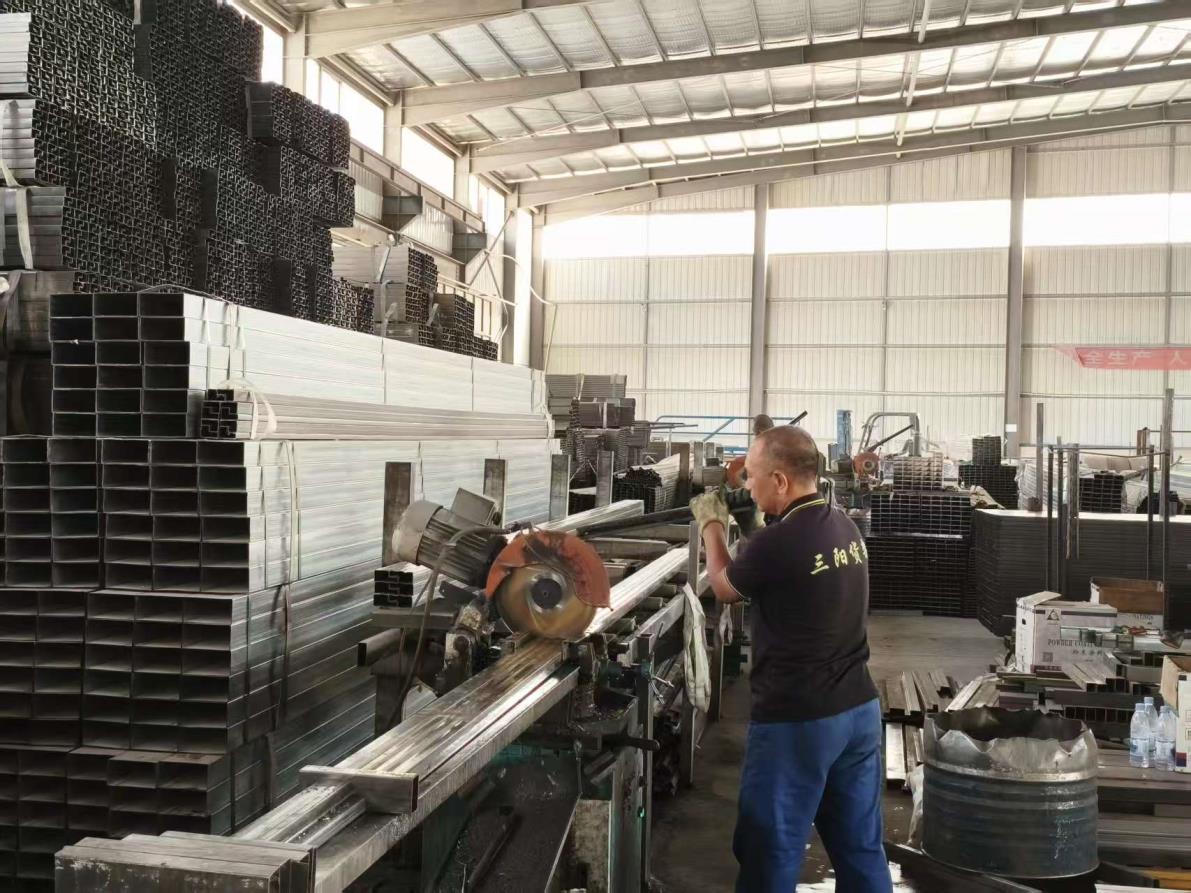
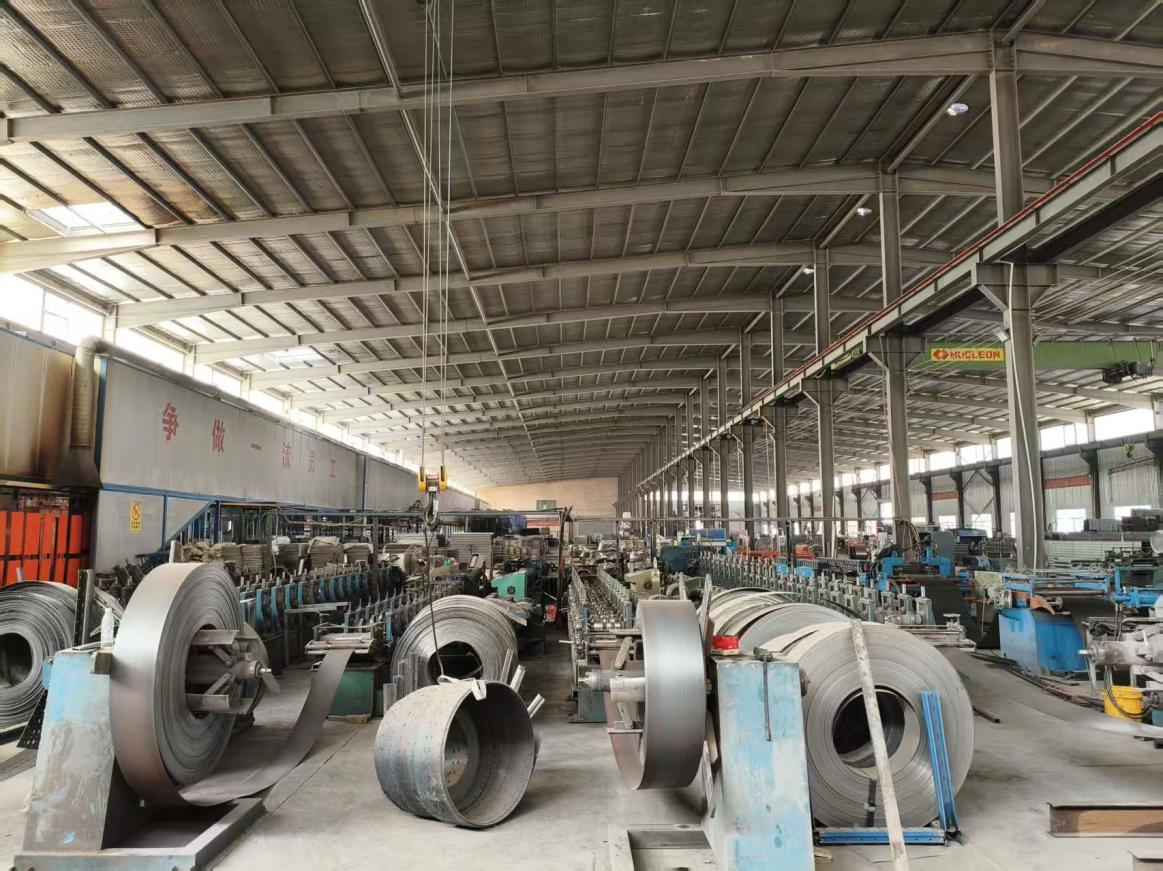
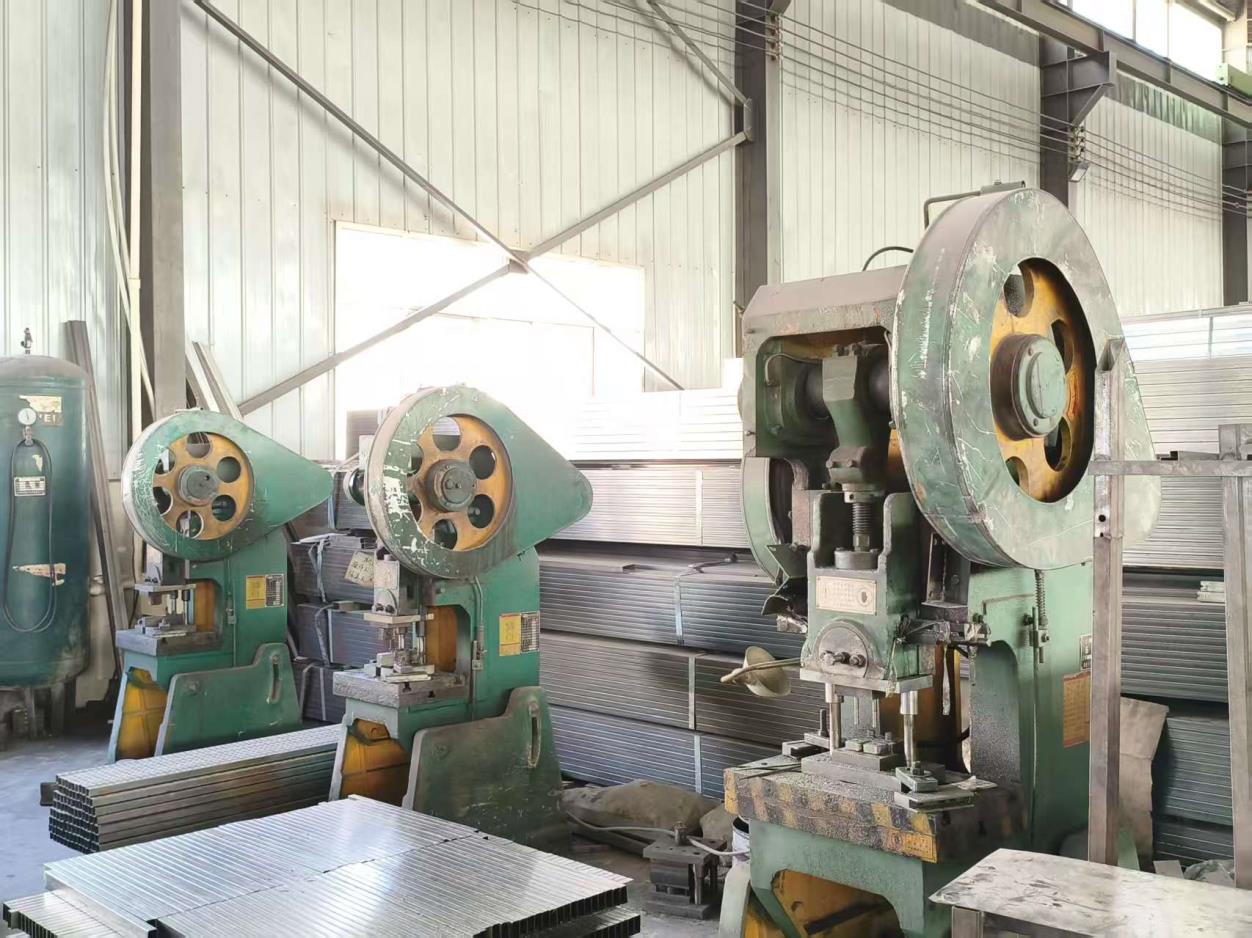
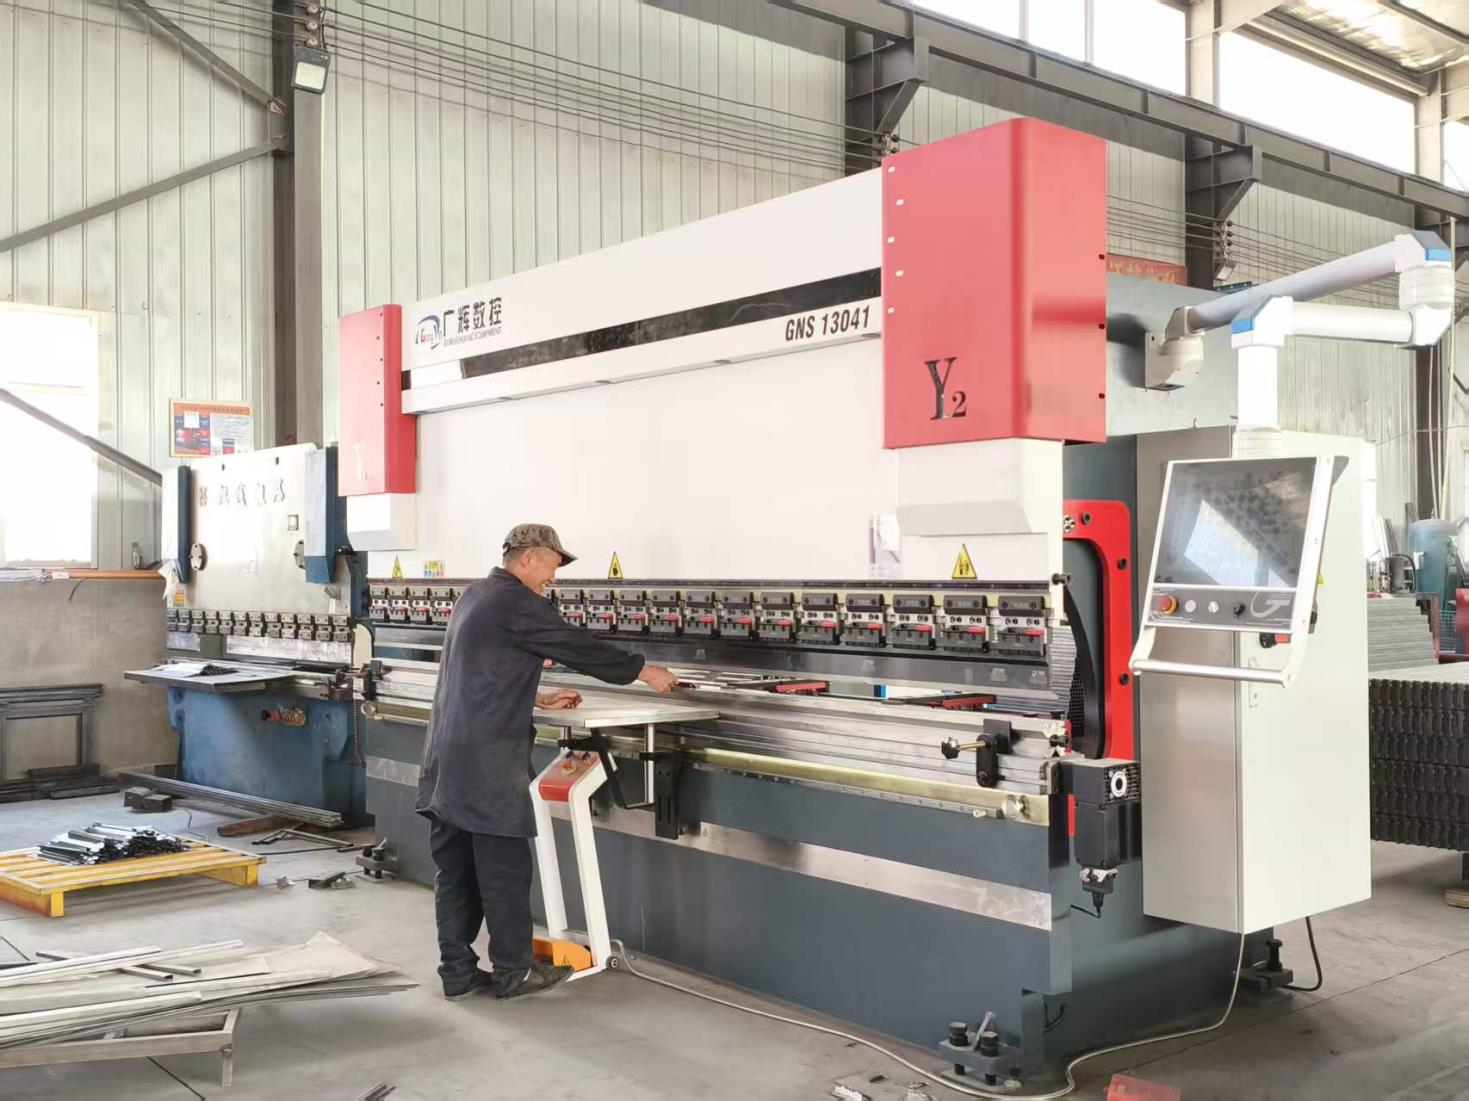
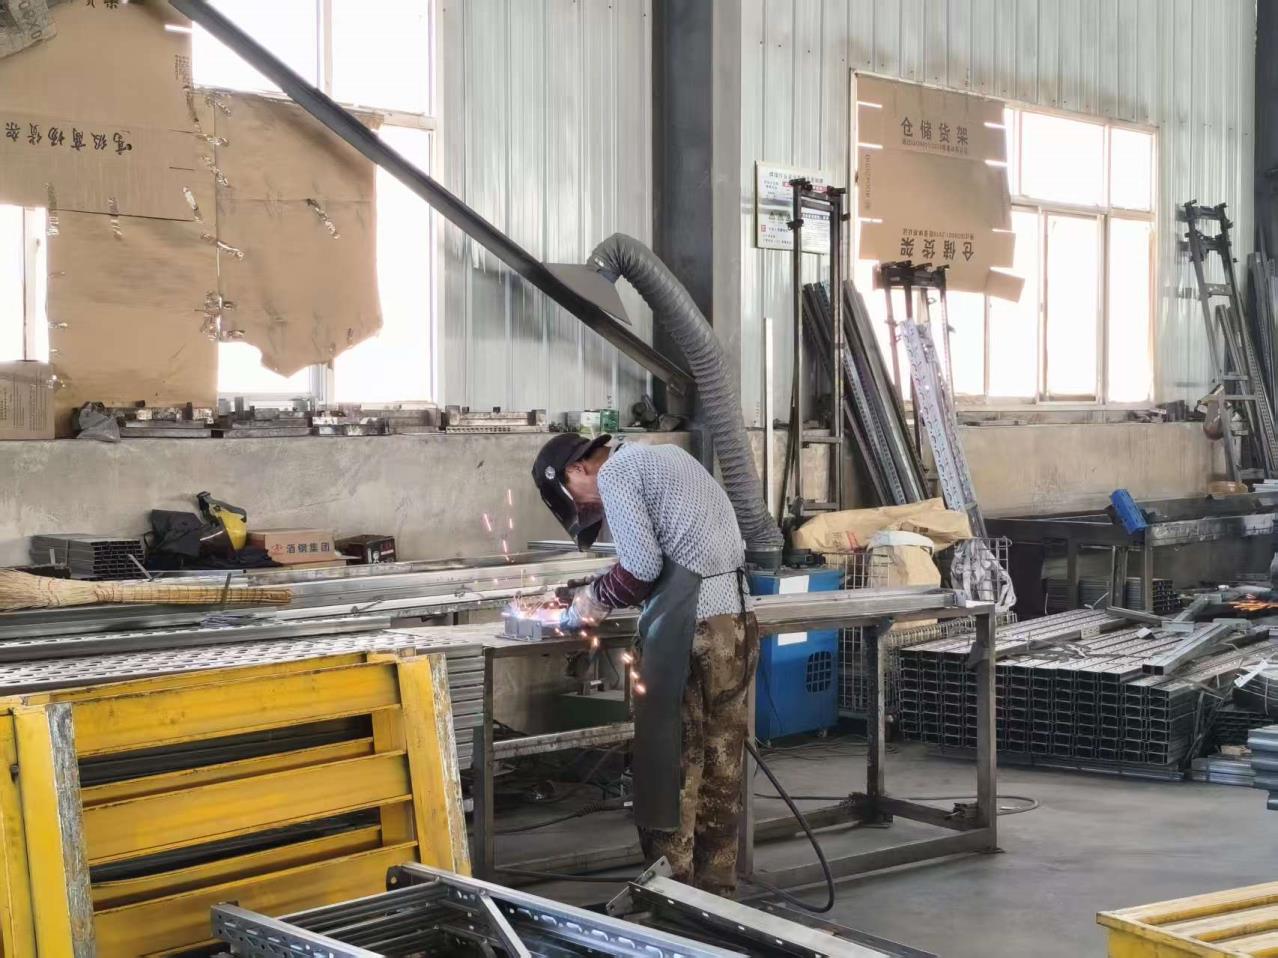
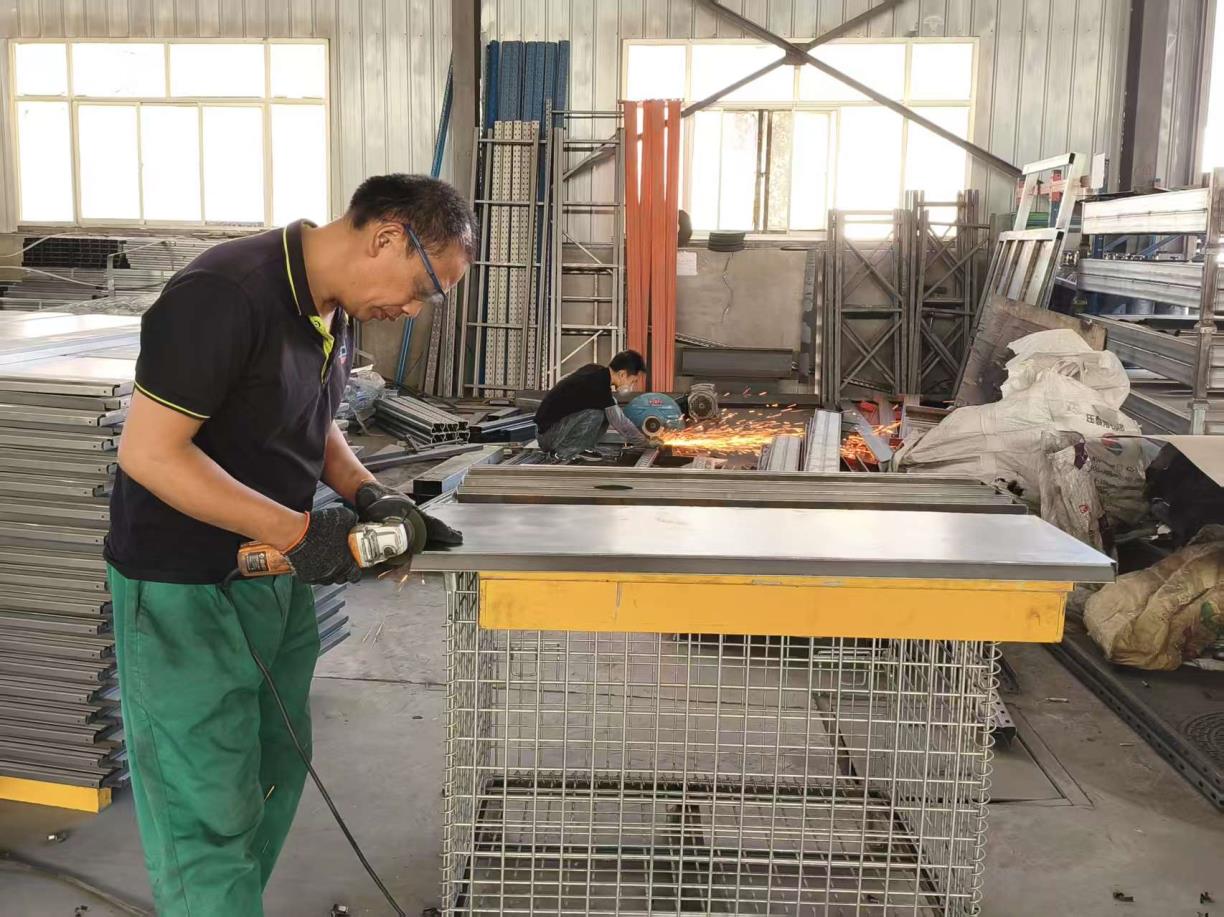
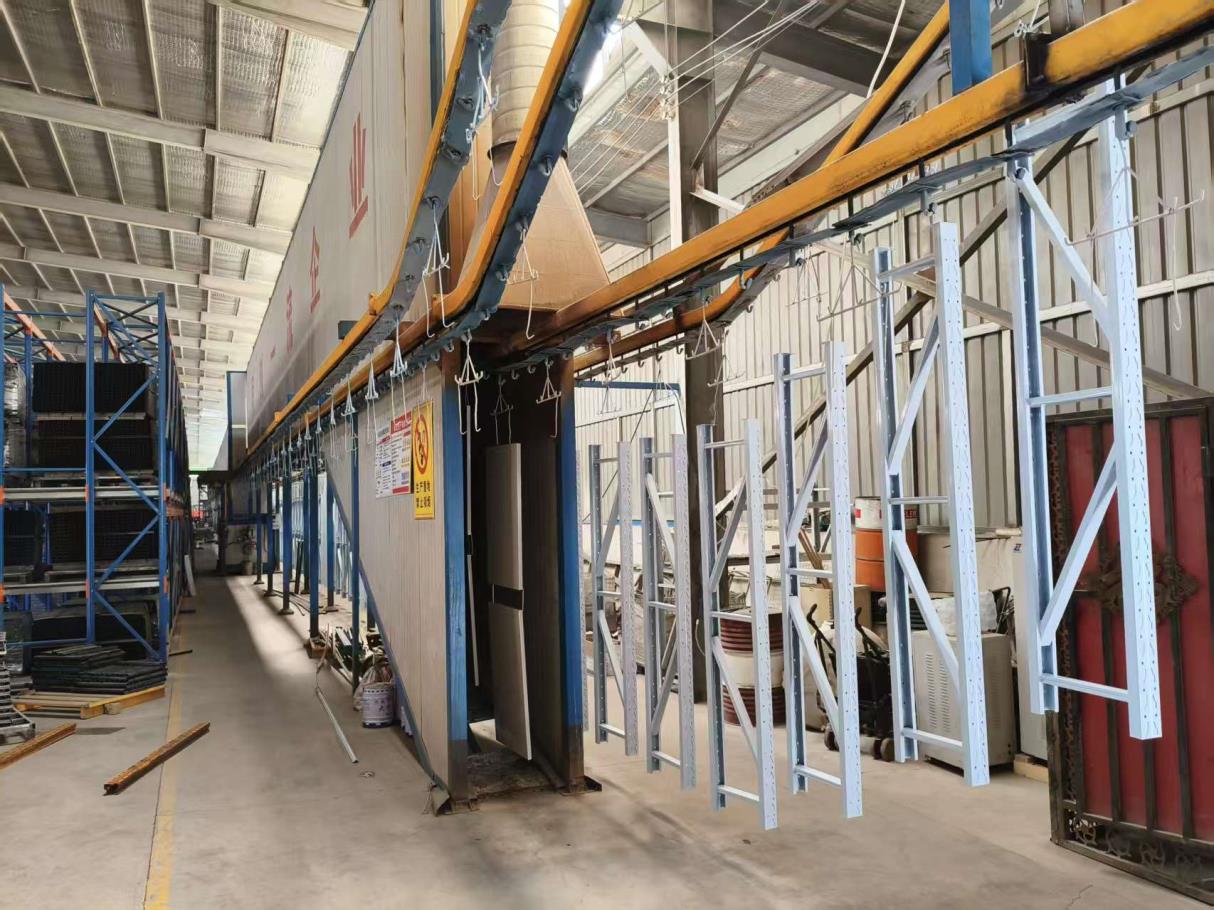
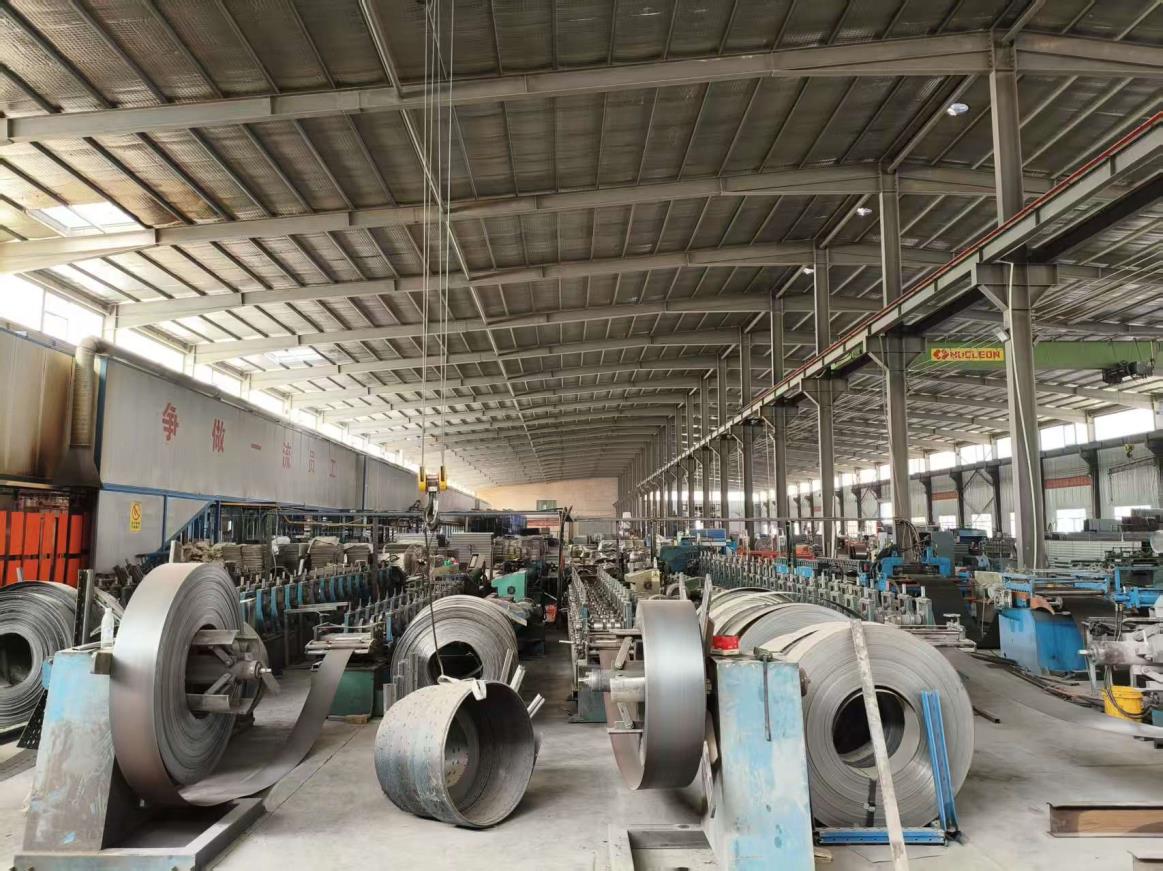
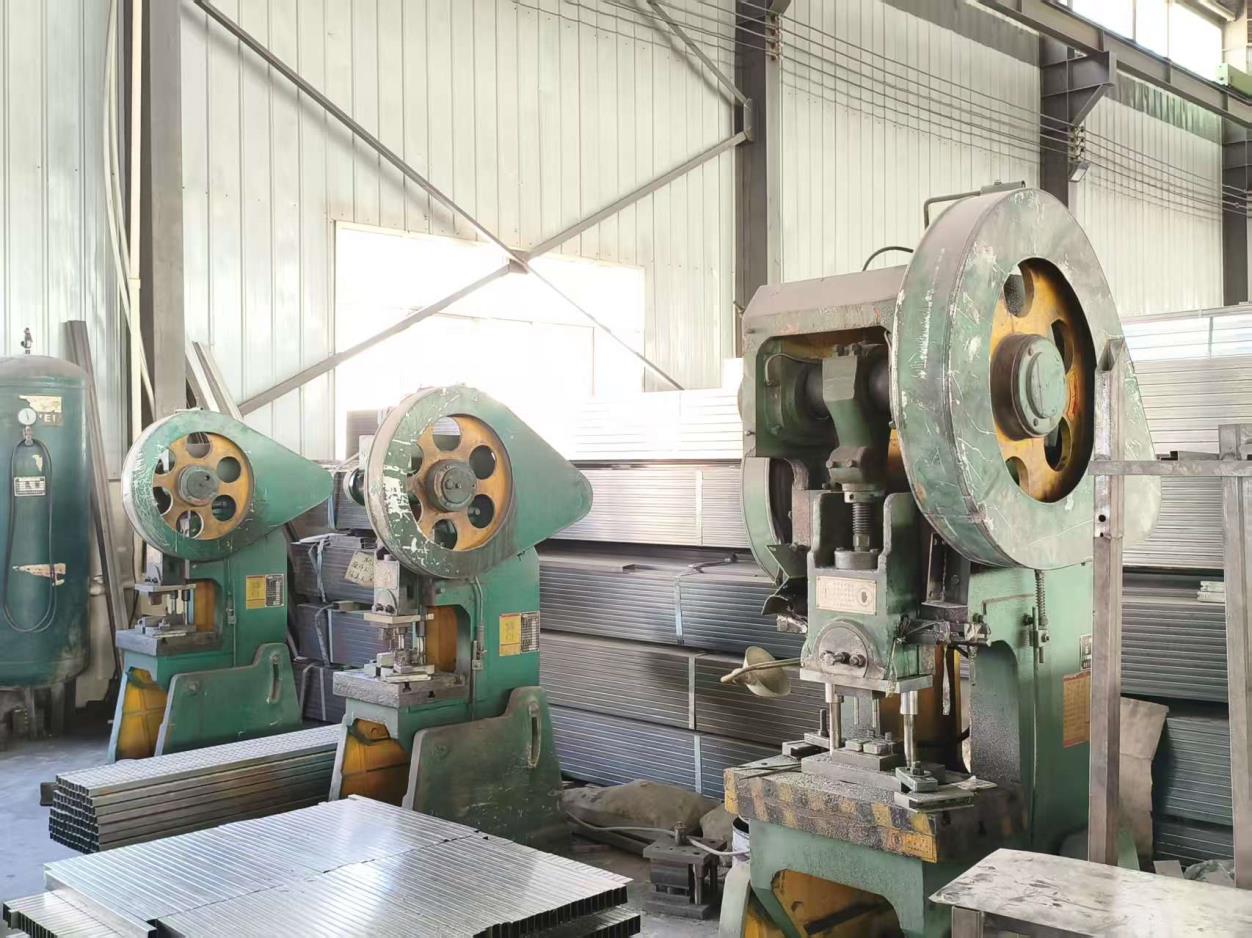
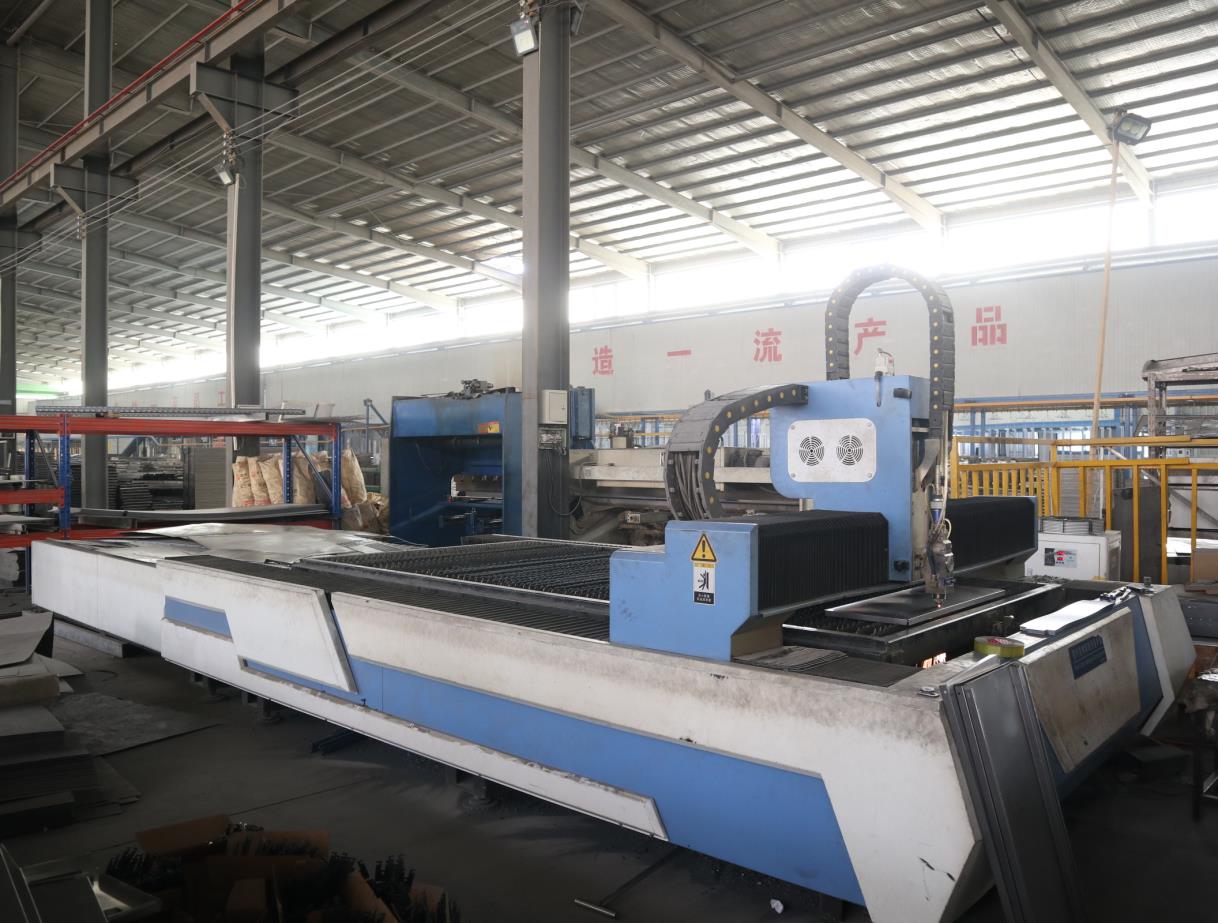
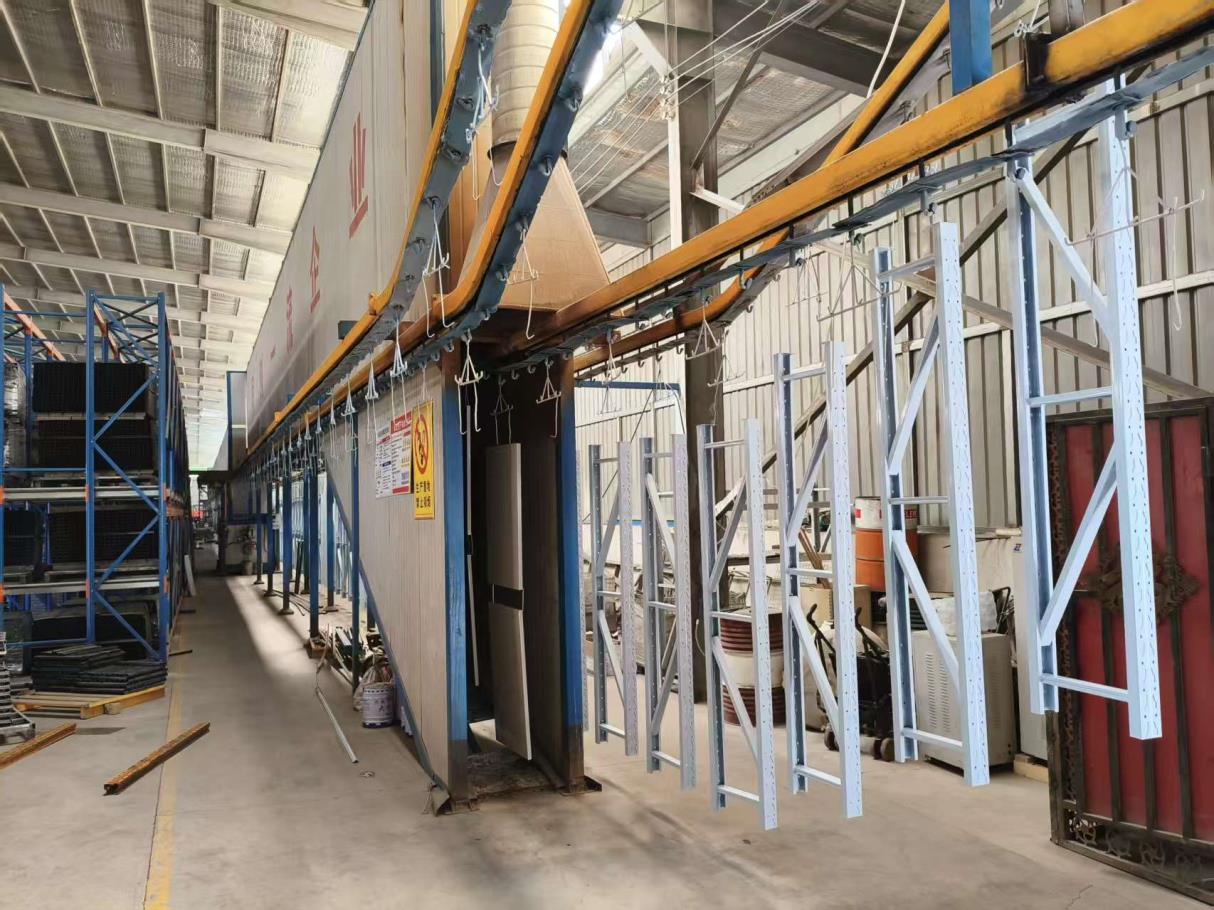
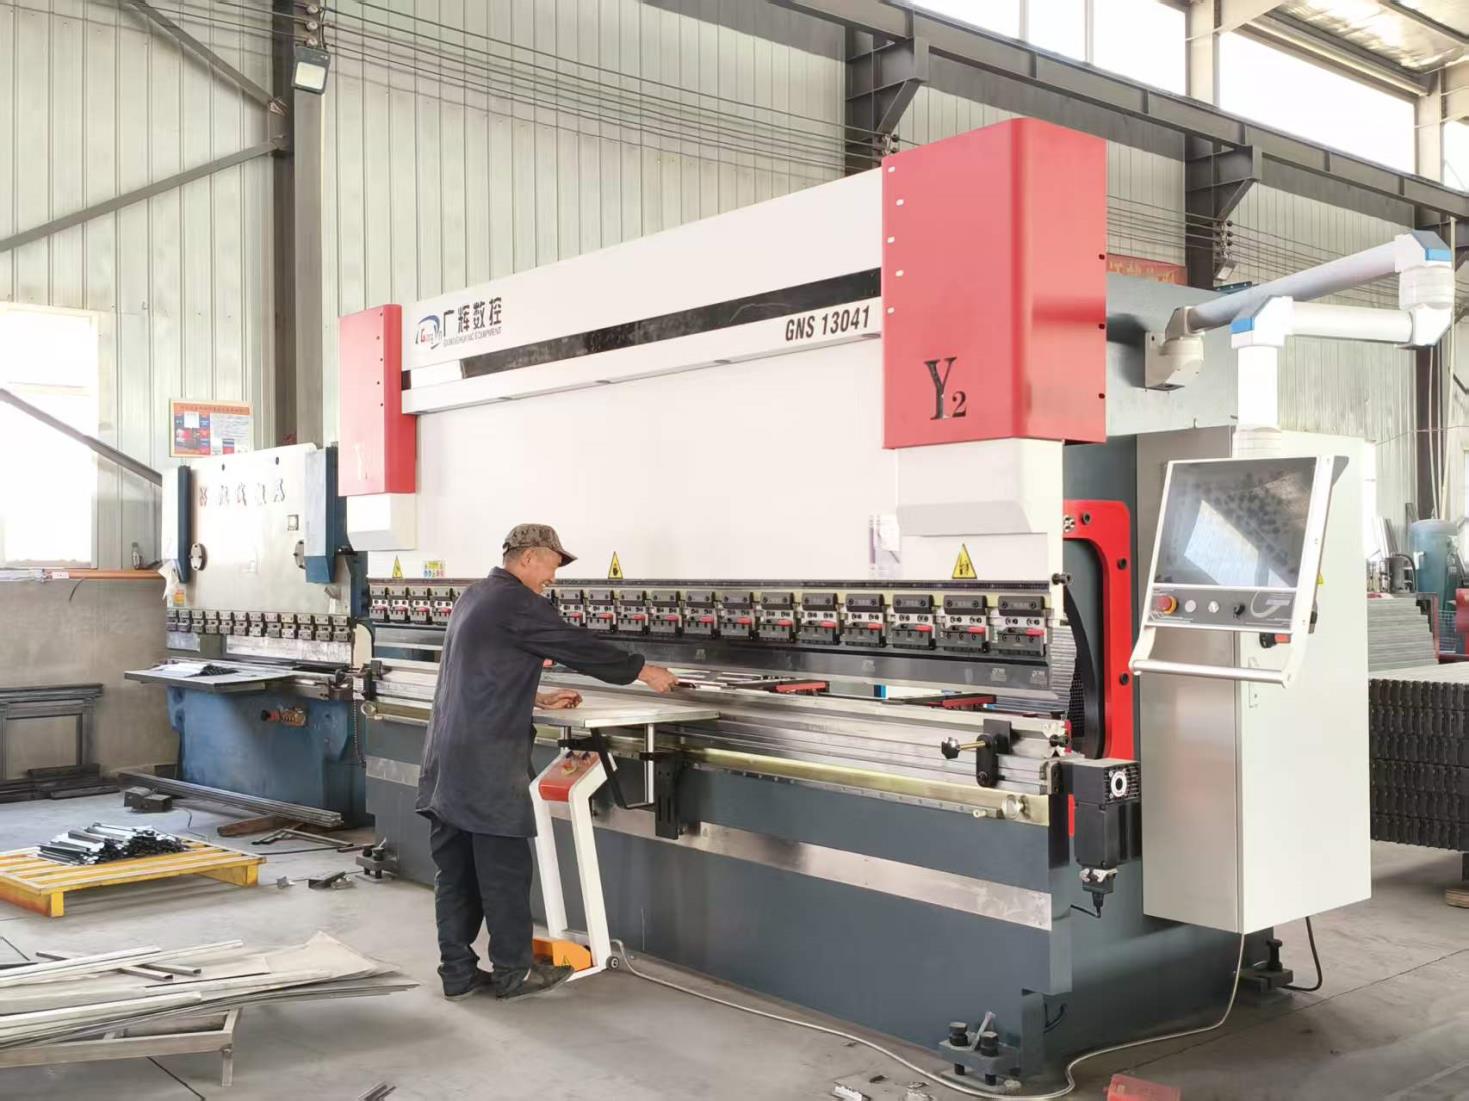
Unlike factories relying on secondary subcontracting, China's modern manufacturing hubs house the entire process in-house: from automated cold rolling and high-frequency punching to robotized welding and eco-friendly electrostatic powder-coating. Automated cold-rolling ensures structural consistency across all upright frames and beams, allowing for precise grid adjustments and long-term modular layout stability.
With an engineering cohort featuring 68 R&D technicians, modern manufacturers utilize CAD/BIM floor layouts and advanced FEA simulations. This technology identifies load-stress points, predicts seismic reactions, and calculates exact weight distributions. Retail operations benefit from precise structural profiles optimized to reduce material weight without sacrificing loading capacity, lowering ocean freight costs and minimizing the physical footprint on the retail floor.
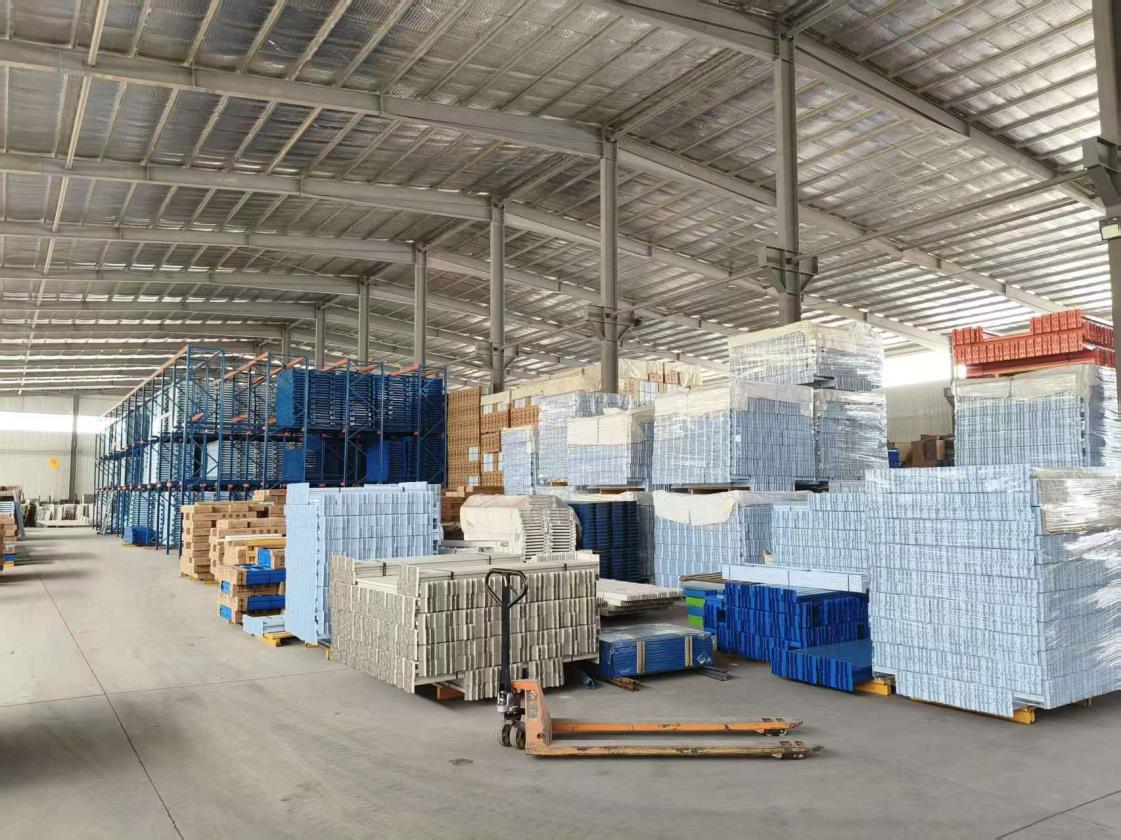
From raw Q235B steel coils to finished powder-coated display and warehousing systems, our production line guarantees structural accuracy and durability.
Retail configurations vary significantly depending on region, footprint size, product variety, and dynamic consumer flow. Designing modular display layouts requires matching the shelving system to the target customer's purchasing journey.
Maximizes vertical spaces using light-duty metal gondolas combined with wood veneer cladding or plastic tag strips. Integrated LED track lighting draws attention to premium display units while preserving walkways.
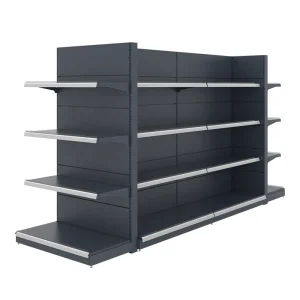
Utilizes heavy-duty double-sided modular runs. Built to handle loading capacities up to 150kg per shelf level, these configurations feature adjustable pitch configurations and specialized pricing modules.
Combines standard retail display shelving with industrial warehouse pallet racking systems. Utilizes structural hot-dip galvanized parts to resist moisture and rust in cold-chain and sub-zero storage environments.
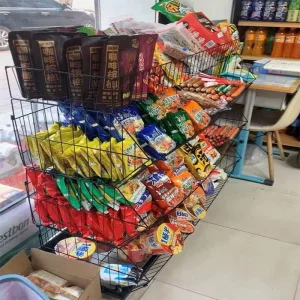
In addition, checkout pathways are optimized using motorized cash wraps and custom-sized counter systems. Matching display shelves to customer queues minimizes waiting times, improves security, and drives impulse purchases through strategically placed snack, candy, and convenience displays.
The supermarket shelving industry is shifting from static steel platforms toward intelligent, adaptive display modules. The following key trends are shaping high-density retail design:
Digital price tag integration is standard in modern retail rollouts. Shelves are fabricated with custom-fit plastic rail profiles and integrated routing paths to power digital display units, minimizing manual price change tasks and improving price labeling accuracy.
Commercial operators require store fixtures with low environmental impact. Eco-friendly manufacturing lines use lead-free, VOC-free epoxy polyester powder coatings. Electrostatic application processes ensure thick protective barriers that resist impacts and chemical wear, extending the working life of the steel structure.
Modern layouts change along with seasonal promotions and fast-moving inventory trends. Toolless snap-in bracket assemblies enable in-store staff to adjust height margins, switch between double-sided hooks and wire baskets, or reposition end-caps without requiring specialized structural installation tools.
Procuring commercial equipment from overseas factories requires careful verification of quality assurance and structural engineering protocols. Importers should verify the following indicators prior to initiating large-scale orders:
Nanjing Dulis (DuraRacks) ensures these benchmarks are met through a 45-person QA department. The team performs raw-material weld checks, mechanical tensile testing, and structural inspections on every batch, ensuring compliance with global specifications.
Answers to common structural engineering, custom order, and export delivery questions from global procurement agents.
Established in 2014, Nanjing Dulis Warehouse Equipment Co., Ltd. (operating globally under the brand DuraRacks) is a premier industrial rack manufacturer headquartered in Nanjing, China. Boasting over 12 years of industry experience and 9 years of direct export experience, our facility spans a modern industrial building area of 38,000 square meters. We specialize in high-capacity pallet racking, drive-in systems, and automated storage solutions, generating an annual export revenue of $32 million USD.
Quality Assurance & Testing Standards: Quality and structural integrity form the bedrock of our manufacturing philosophy. Our dedicated team of 45 certified QA personnel implements rigorous quality control processes aligned with ISO9001, CE, and FEM standards. Every batch undergoes comprehensive product inspection methods, including ultrasonic weld flaw detection, mechanical tensile testing, static and dynamic load capacity testing, and salt spray corrosion resistance evaluation.
Global Trade & Supply Chain: Supported by a robust network of over 1,200 qualified supply chain partners, DuraRacks operates as an integrated direct-export manufacturer. Our primary overseas markets encompass North America, Western Europe, and Australia. We serve a diverse portfolio of client types, primarily catering to 3PL logistics hubs, large-scale e-commerce fulfillment centers, cold storage operations, and heavy industrial manufacturing plants.
R&D & Customization Capabilities: Driven by an experienced team of 68 R&D engineers, DuraRacks delivers advanced structural Finite Element Analysis (FEA) and customized CAD/BIM warehouse layout simulations. We offer full OEM/ODM customization options, tailored seismic load engineering, special powder-coating finishes, and custom beam profile dimensions. Last year alone, our engineering team launched 85 new product innovations and patented racking components, ensuring cutting-edge storage efficiency for our global clientele.
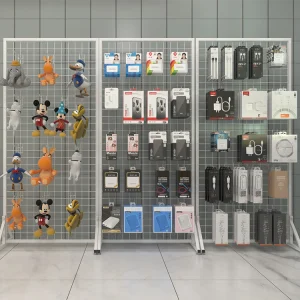
Explore our specialized retail accessories, structural wire fixtures, double-sided food gondolas, and heavy-duty storage racks.
 DuraRacks